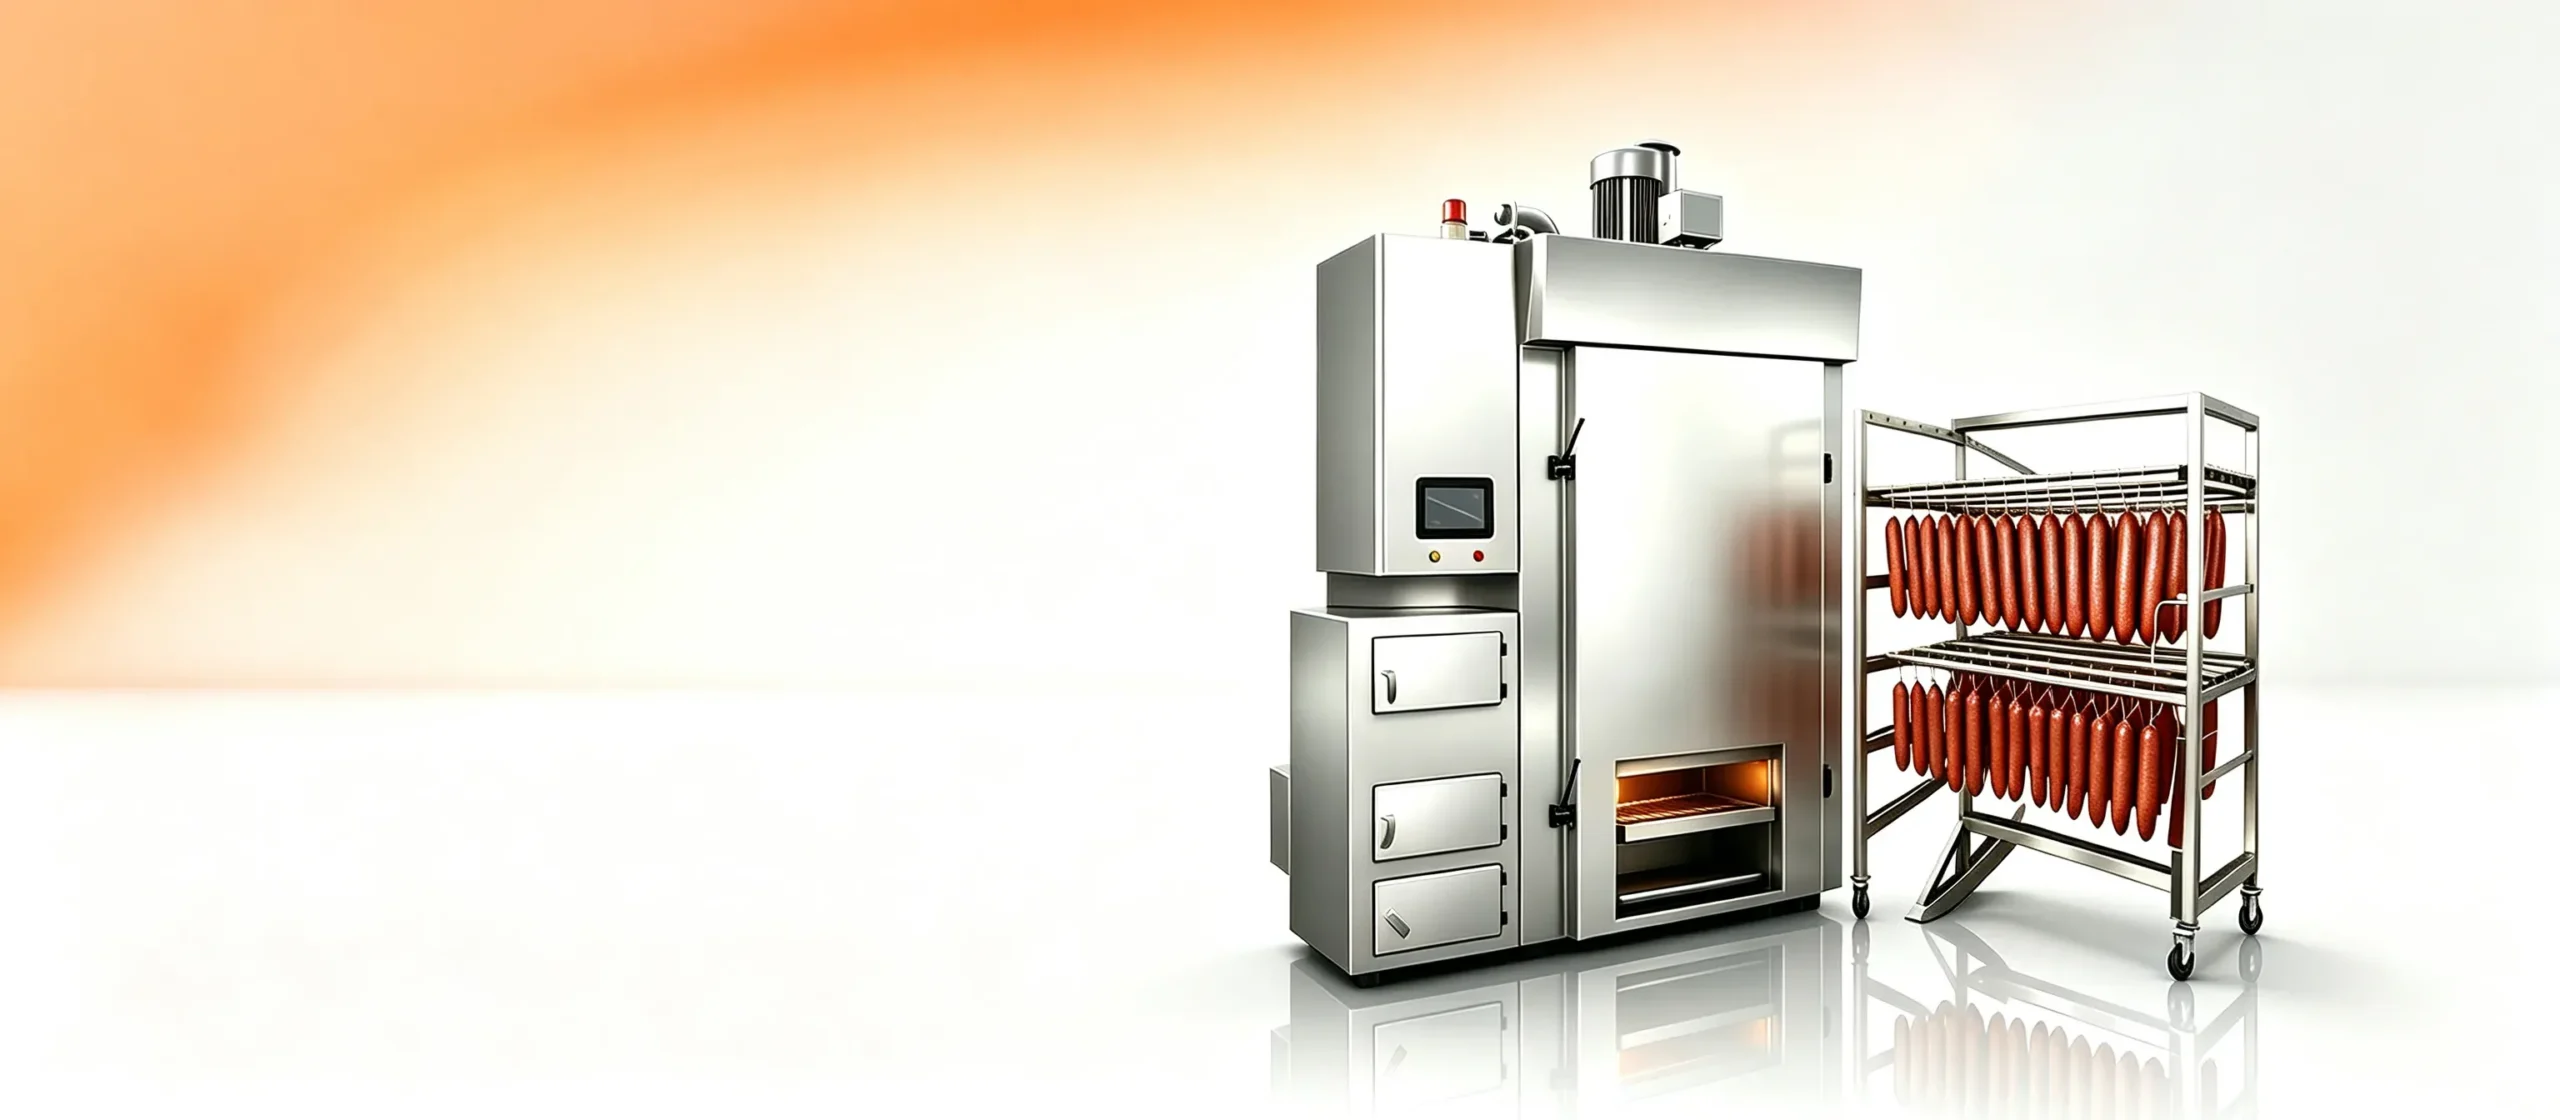
Running a collagen casing sausage line at scale means one constraint towers above all others: air. A single void trapped inside a casing link undermines texture, reduces shelf life, and sends product back through rework. At throughputs approaching 6,500 kg per hour, even a 0.3-second mechanical hesitation can generate hundreds of defective units. This article breaks down exactly how modern vacuum sausage filling machines eliminate air entrainment — and what your production team needs to configure correctly to sustain that output without compromising casing integrity.
Why Air Pockets Form in Collagen Casing Filling
Collagen casings behave differently from natural gut or fibrous casings. Their consistent diameter and controlled permeability make them ideal for high-speed automated lines, but that same consistency means they tolerate zero margin for erratic filling pressure. Air pockets originate from several overlapping mechanical and process causes that compound one another during continuous operation.
Inconsistent Feed Pressure
Fluctuating pump pressure allows brief pressure drops where meat paste separates from the nozzle wall, drawing air inward before the casing seals.
Meat Temperature Variance
Partially thawed blocks introduce viscosity shifts mid-batch. Denser cold zones create localized voids as the paste fails to fully displace air ahead of it.
Hopper Re-loading Gap
Manual top-loading introduces air between fresh and remaining paste. Without continuous vacuum, that air migrates to the filling nozzle within seconds.
Rotor Clearance Wear
As vane or piston components wear, clearance between rotor and housing widens, allowing compressed air back-flow into the fill chamber during the discharge stroke.
How Vane-Type Vacuum Filling Eliminates Air Entrainment
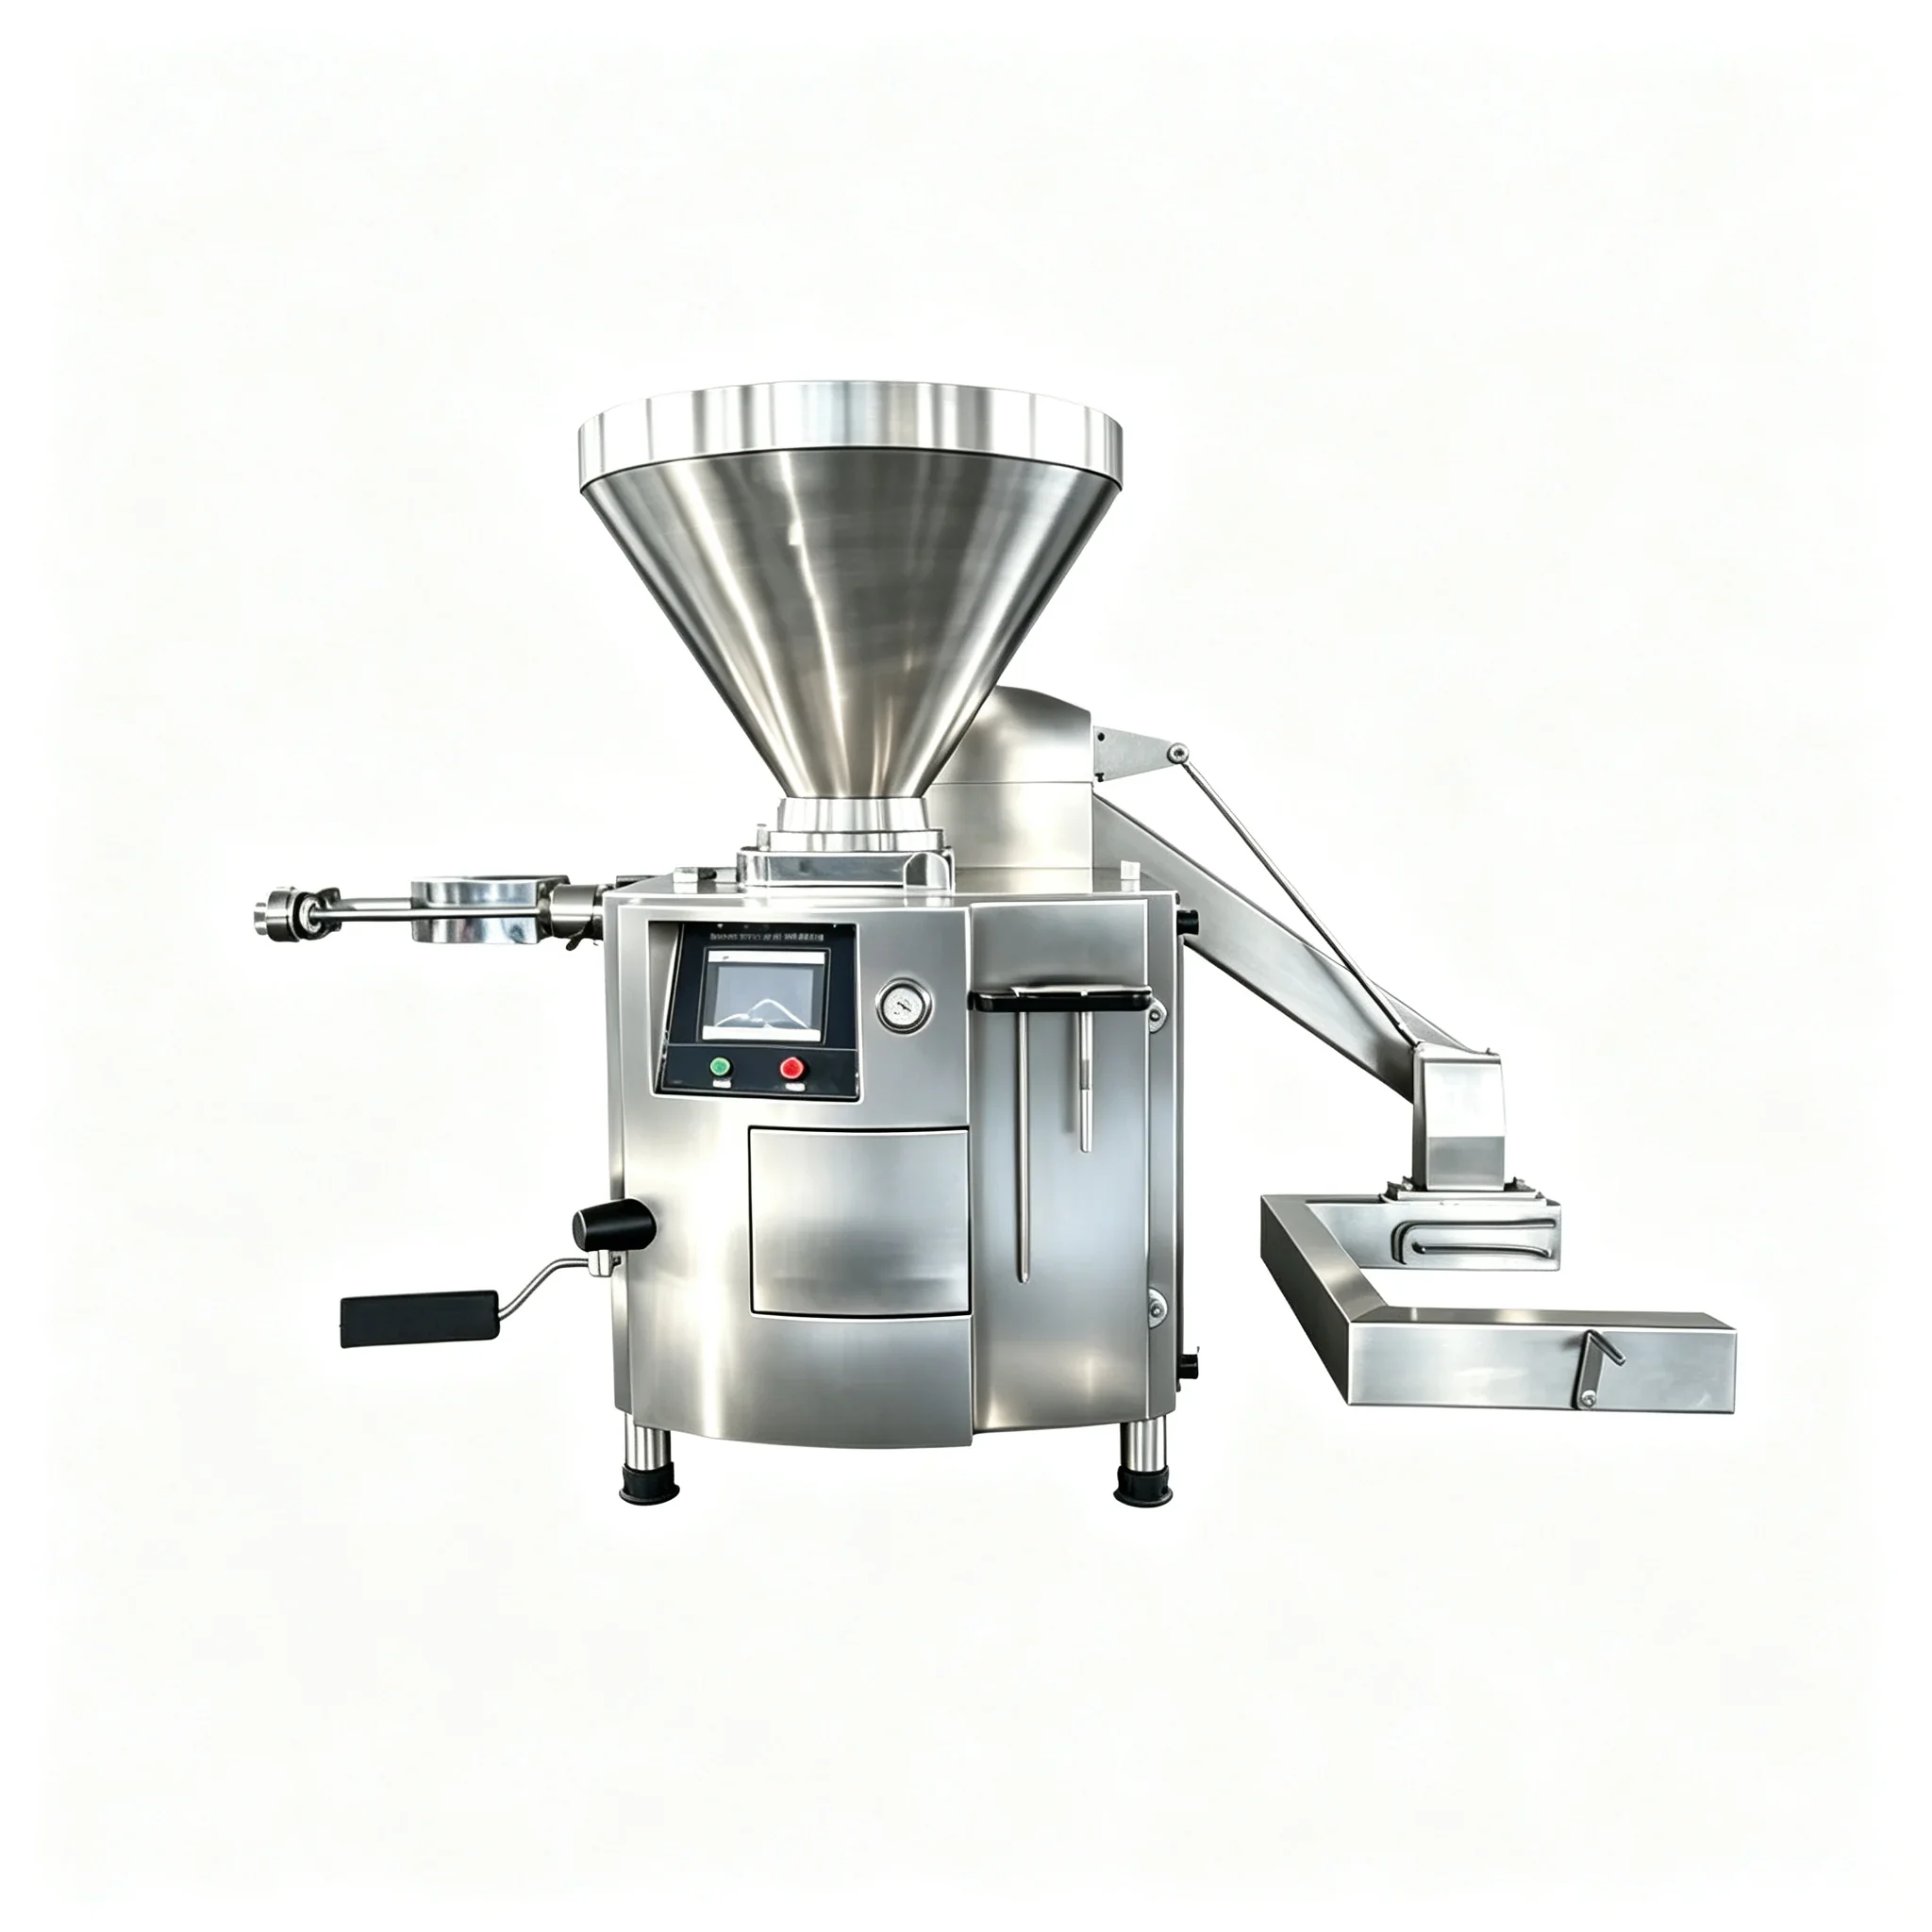
The core engineering principle behind a vane-type vacuum filling machine is displacement without compression. Rather than forcing paste through a constriction — which creates turbulence and draws in surrounding air — the rotating vane system creates a series of sealed chambers that carry fixed volumes of meat paste from the hopper to the nozzle in a continuous, uninterrupted sequence. This volumetric principle is what makes high-speed collagen casing filling physically achievable at 6,500 kg/h.
The Dual-Stage Vacuum System
A properly configured vacuum sausage filler operates two distinct vacuum stages simultaneously. The first stage degasses the meat paste inside the hopper before it contacts the vane rotor — removing dissolved and mechanically entrained gases that accumulated during mixing or tumbling. The second stage maintains a controlled low-pressure environment within the fill chamber itself, so any residual micro-bubbles are drawn out before the paste exits the nozzle. Together, these stages reduce void content in finished collagen casing links to below 0.1% by volume under normal operating conditions.
Constant Pressure at the Nozzle
Achieving 6,500 kg/h without air pockets demands pressure stability at the stuffing horn of ±0.02 bar or better across the full operating cycle. The ZKG-6500 platform achieves this through servo-controlled vane speed, which compensates for paste viscosity changes in real time. When meat temperature drops — common at the start of a new hopper load — the servo increases rotor torque proportionally, maintaining volumetric output without creating the low-pressure transients that allow air ingestion. This is fundamentally different from older hydraulic-piston designs, which produce sinusoidal pressure curves and corresponding void cycles.
Breaking Down 6,500 kg/h: What the Numbers Actually Mean
A throughput rating of 6,500 kg/h is a maximum figure under ideal conditions — but understanding what drives it, and where losses occur, is what separates a plant that hits that number consistently from one that only sees it during commissioning. The table below maps the key variables that directly affect realized throughput on a collagen casing line.
| Variable | Optimal Range | Impact on Throughput | Air Pocket Risk |
|---|---|---|---|
| Meat paste temperature | −2°C to +2°C | ±8% variation | High above +4°C |
| Vacuum level (hopper) | −0.08 to −0.09 MPa | Minimal direct | Critical — primary control |
| Casing caliber | 18–38 mm collagen | ±15% variation | Medium at extremes |
| Nozzle diameter match | ≤80% of casing ID | ±10% variation | High if mismatched |
| Vane rotor speed | Servo-adjusted (auto) | Direct linear relation | Low (servo-controlled) |
| Hopper refill method | Continuous (T200 lift) | Up to −18% if manual | High during changeover |
The figures above confirm that vacuum level and refill method are the two variables with the most direct influence on air pocket formation — and both are equipment-configuration decisions, not process discipline issues. A plant running manual hopper loading on a 6,500 kg/h capable machine is effectively operating at 5,300 kg/h realized output while introducing defect risks during every changeover. Pairing the vacuum filler with a T200 lifting machine eliminates those gaps entirely.
Selecting the Right Sausage Filling Equipment for Your Collagen Casing Line
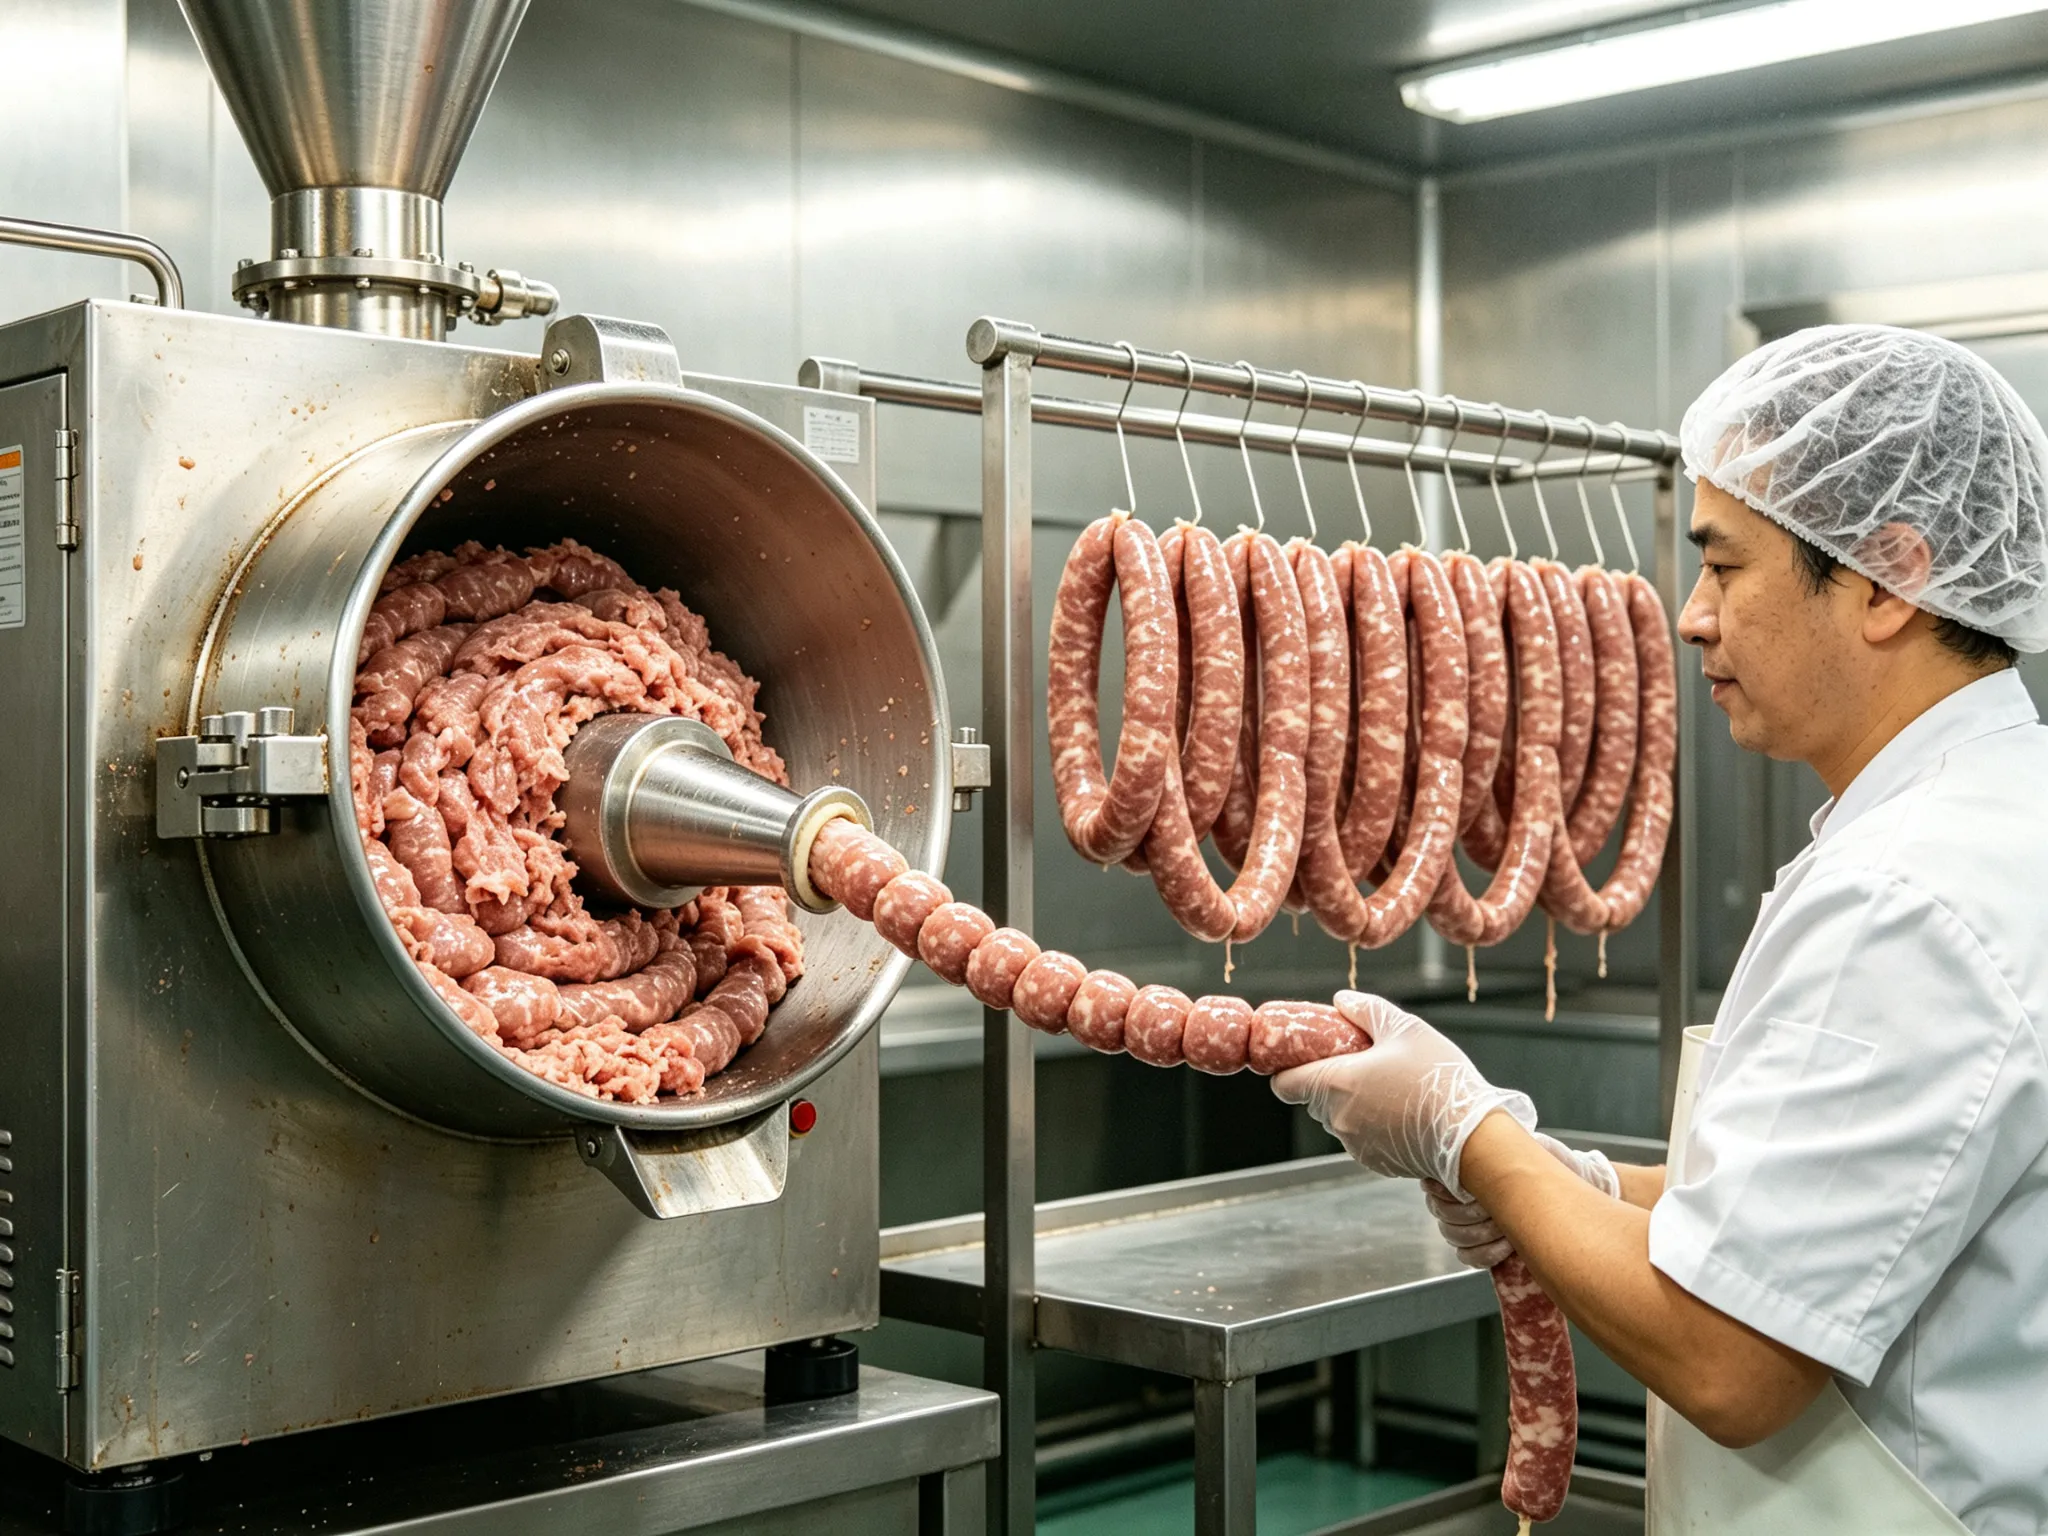
Not every sausage filling machine rated at high capacity is engineered specifically for collagen casing. Natural casing products tolerate minor filling irregularities because gut is elastic and self-sealing; collagen is not. Before specifying a machine, confirm four non-negotiable technical requirements with your supplier.
Vacuum Depth and Stability Rating
The machine specification should state vacuum depth as a sustained figure, not a peak. Sustained vacuum at −0.085 MPa or better across the full rotor speed range is the threshold for reliable collagen casing work. Any machine that achieves target vacuum only at low speeds — then loses 15–20% of vacuum depth at full throughput — will produce intermittent air pockets that are extremely difficult to trace back to the equipment.
Programmable Portioning Accuracy
At 6,500 kg/h with collagen casings, you’re producing upward of 25,000–35,000 links per hour depending on caliber. Portioning accuracy below ±1.5g per link is only achievable with encoder-controlled vane displacement — mechanical cam systems cannot hold this tolerance at sustained high speed. Confirm whether the machine uses pulse-encoder portioning or cam-based portioning before purchasing. The ZKG-6500 platform uses encoder-controlled output, which is what allows consistent sausage casing filling accuracy across the full 6,500 kg/h operating range.
Stainless Steel Contact Surface Standards
All meat-contact surfaces in a high-output collagen casing filling machine must be 304 or 316L stainless steel with surface roughness Ra ≤ 0.8 μm. Rougher surfaces create micro-pockets where paste can stagnate and trap air during the next fill cycle — a source of both voids and bacterial risk. Internal radius transitions at all corners should be minimum 3 mm to eliminate dead zones.
The Complete High-Speed Sausage Production Process Flow
Eliminating air pockets in collagen casing sausage production is not solely a filling-machine problem — it is a line-integration problem. Each upstream and downstream station either contributes to or removes the risk. The sequence below represents best-practice line architecture for a 6,500 kg/h collagen casing operation.
Integrating Vacuum Filling with Automated Sausage Hanging Lines
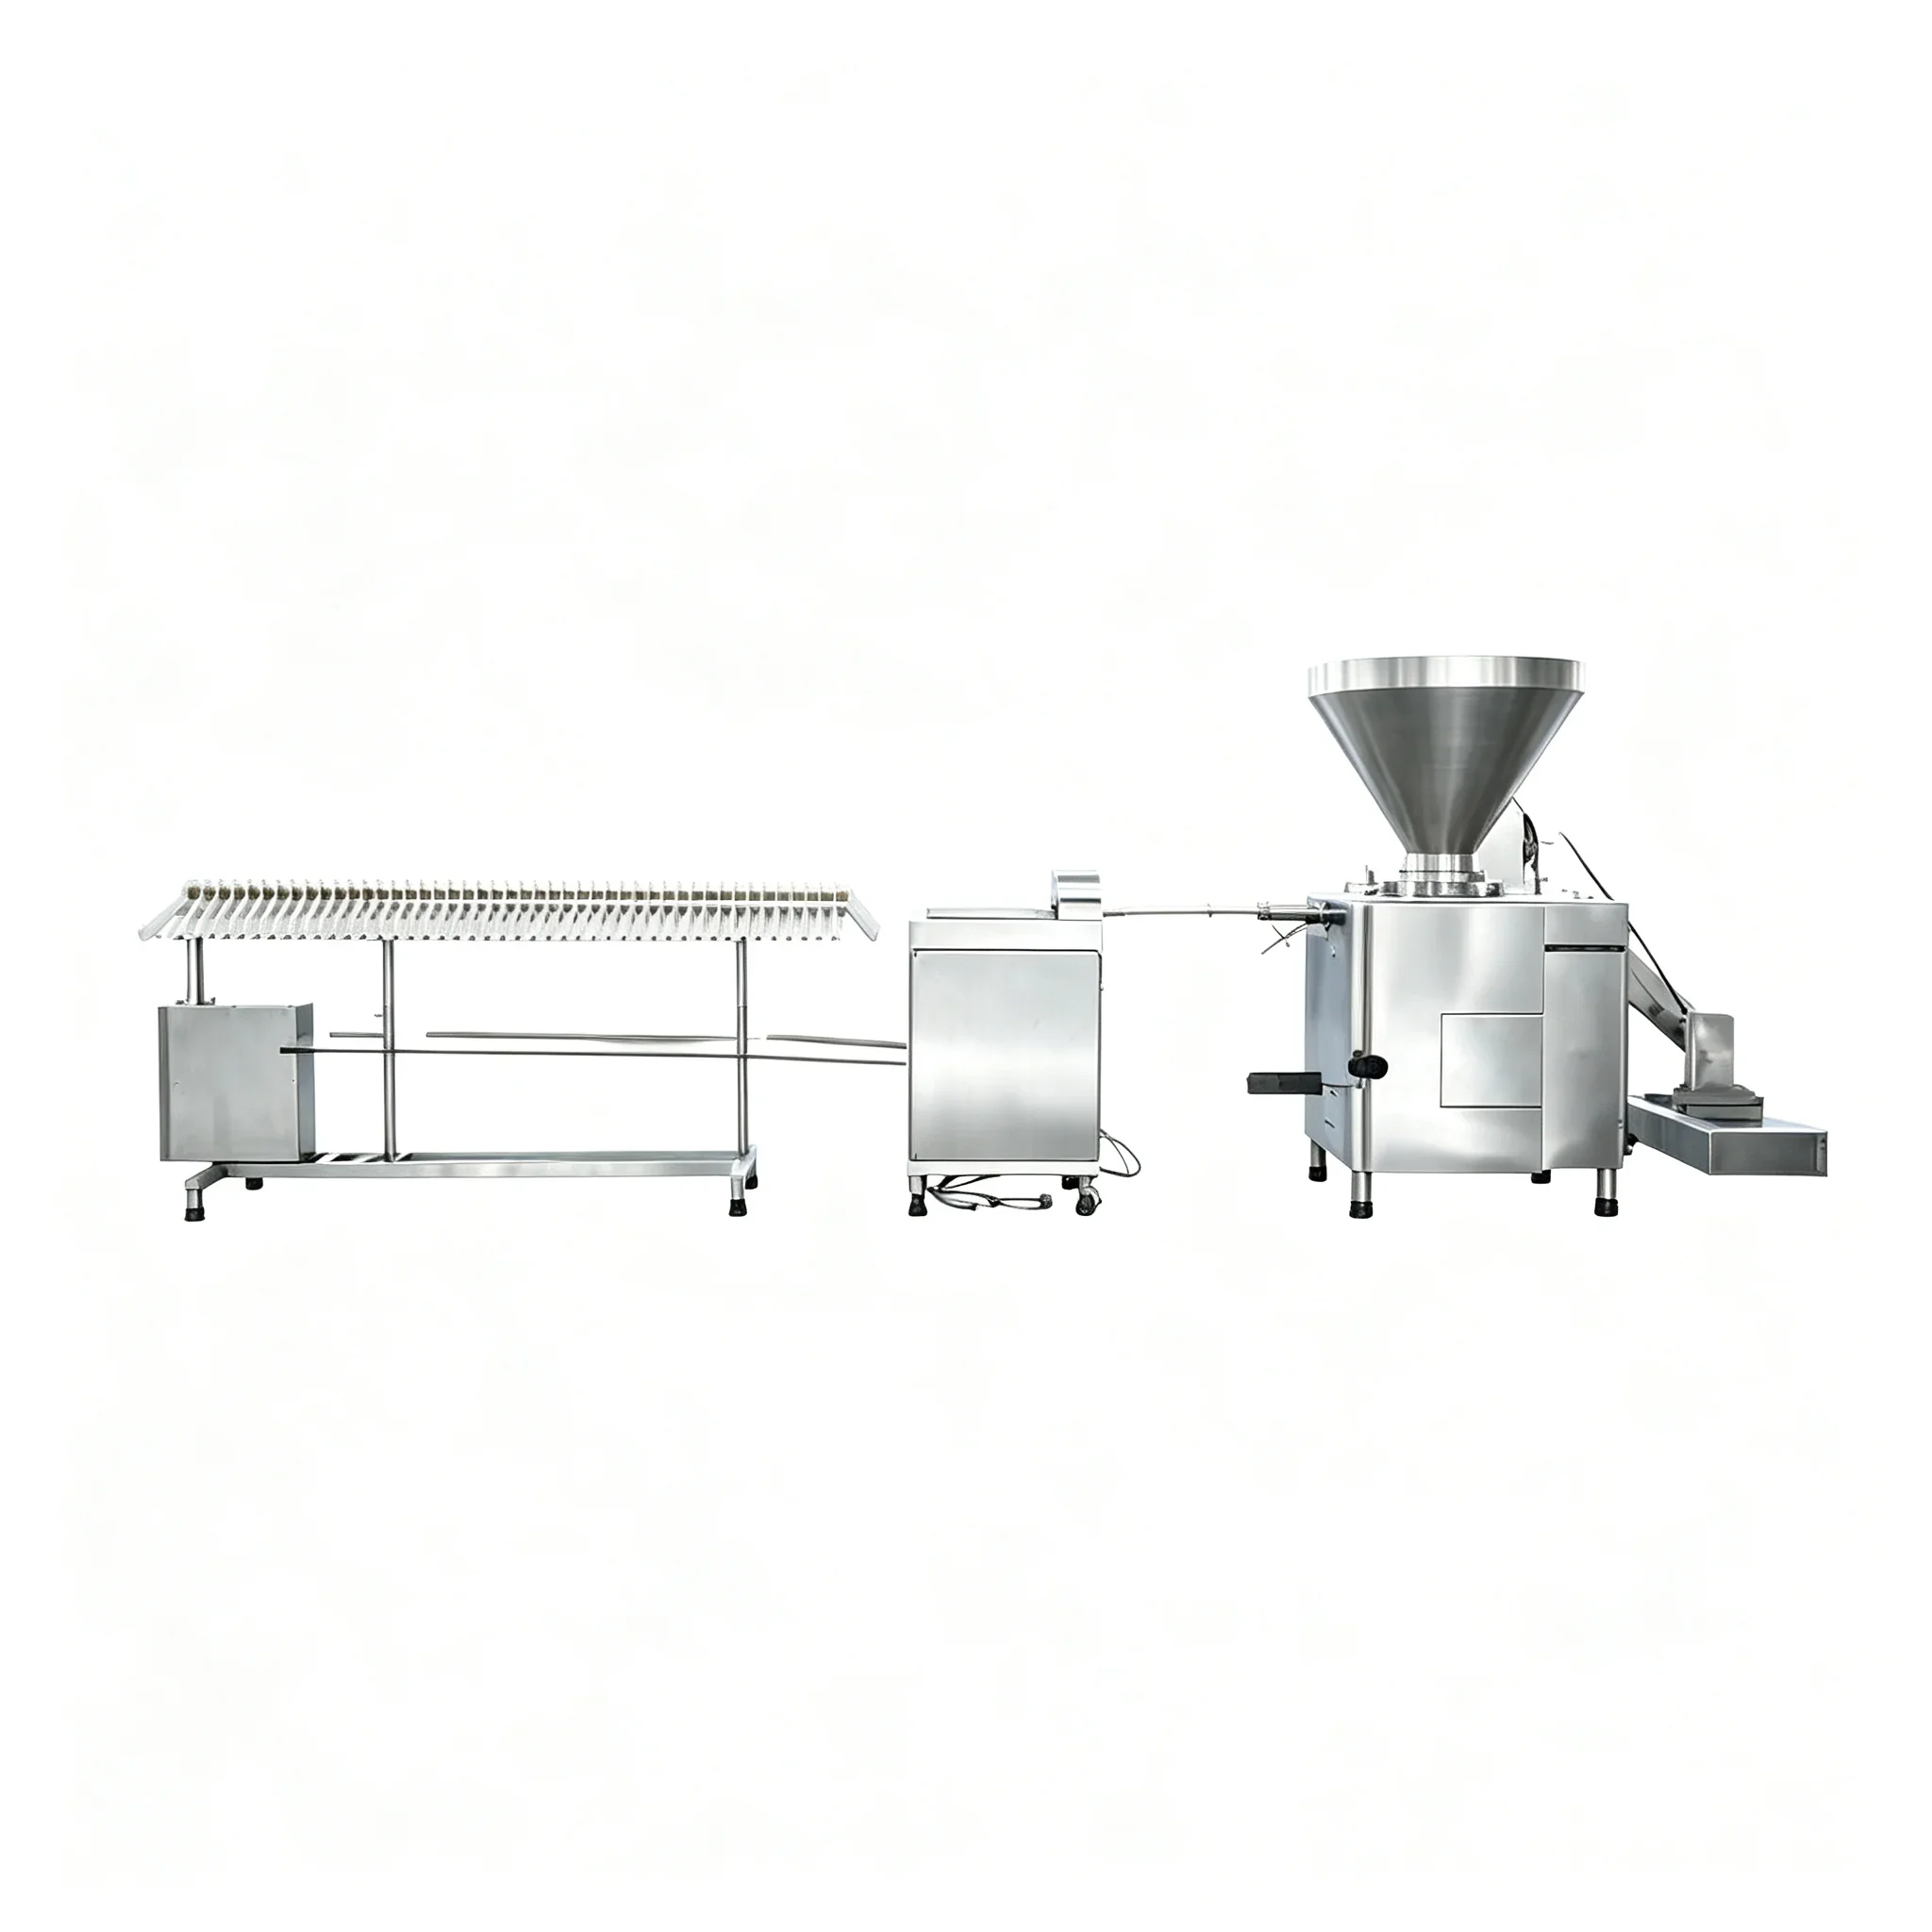
A vacuum filler operating at 6,500 kg/h produces filled casing faster than any manual hanging operation can handle. Without a synchronized automatic sausage linking hanging line, the casing accumulates at the nozzle exit under back-pressure — and that back-pressure is one of the most common causes of air reversal at the stuffing horn. Integration is not optional at this throughput level; it is a prerequisite for air-free filling.
The XDQY high-speed automatic sausage hanging line is designed to accept filled collagen casing from the filler nozzle and advance it at a controlled rate matched to the filler’s output speed. The control interface allows both machines to operate from a single PLC with shared speed reference — when the filler increases throughput by 5%, the hanging line accelerates proportionally, maintaining consistent casing tension and preventing back-pressure buildup at the nozzle.
Link Pitch Consistency Across Calibers
When operating with multiple collagen casing calibers — common in facilities producing both frankfurter and bratwurst formats — the linking pitch must be reconfigured between runs. Modern sausage hanging machines store caliber-specific pitch programs in memory, allowing changeover without mechanical adjustment. This eliminates the trial-and-error link length variation that typically causes the first 50–100 links after a changeover to be inconsistently filled, including with air pockets.
Why Meat Processors Worldwide Choose Our Equipment
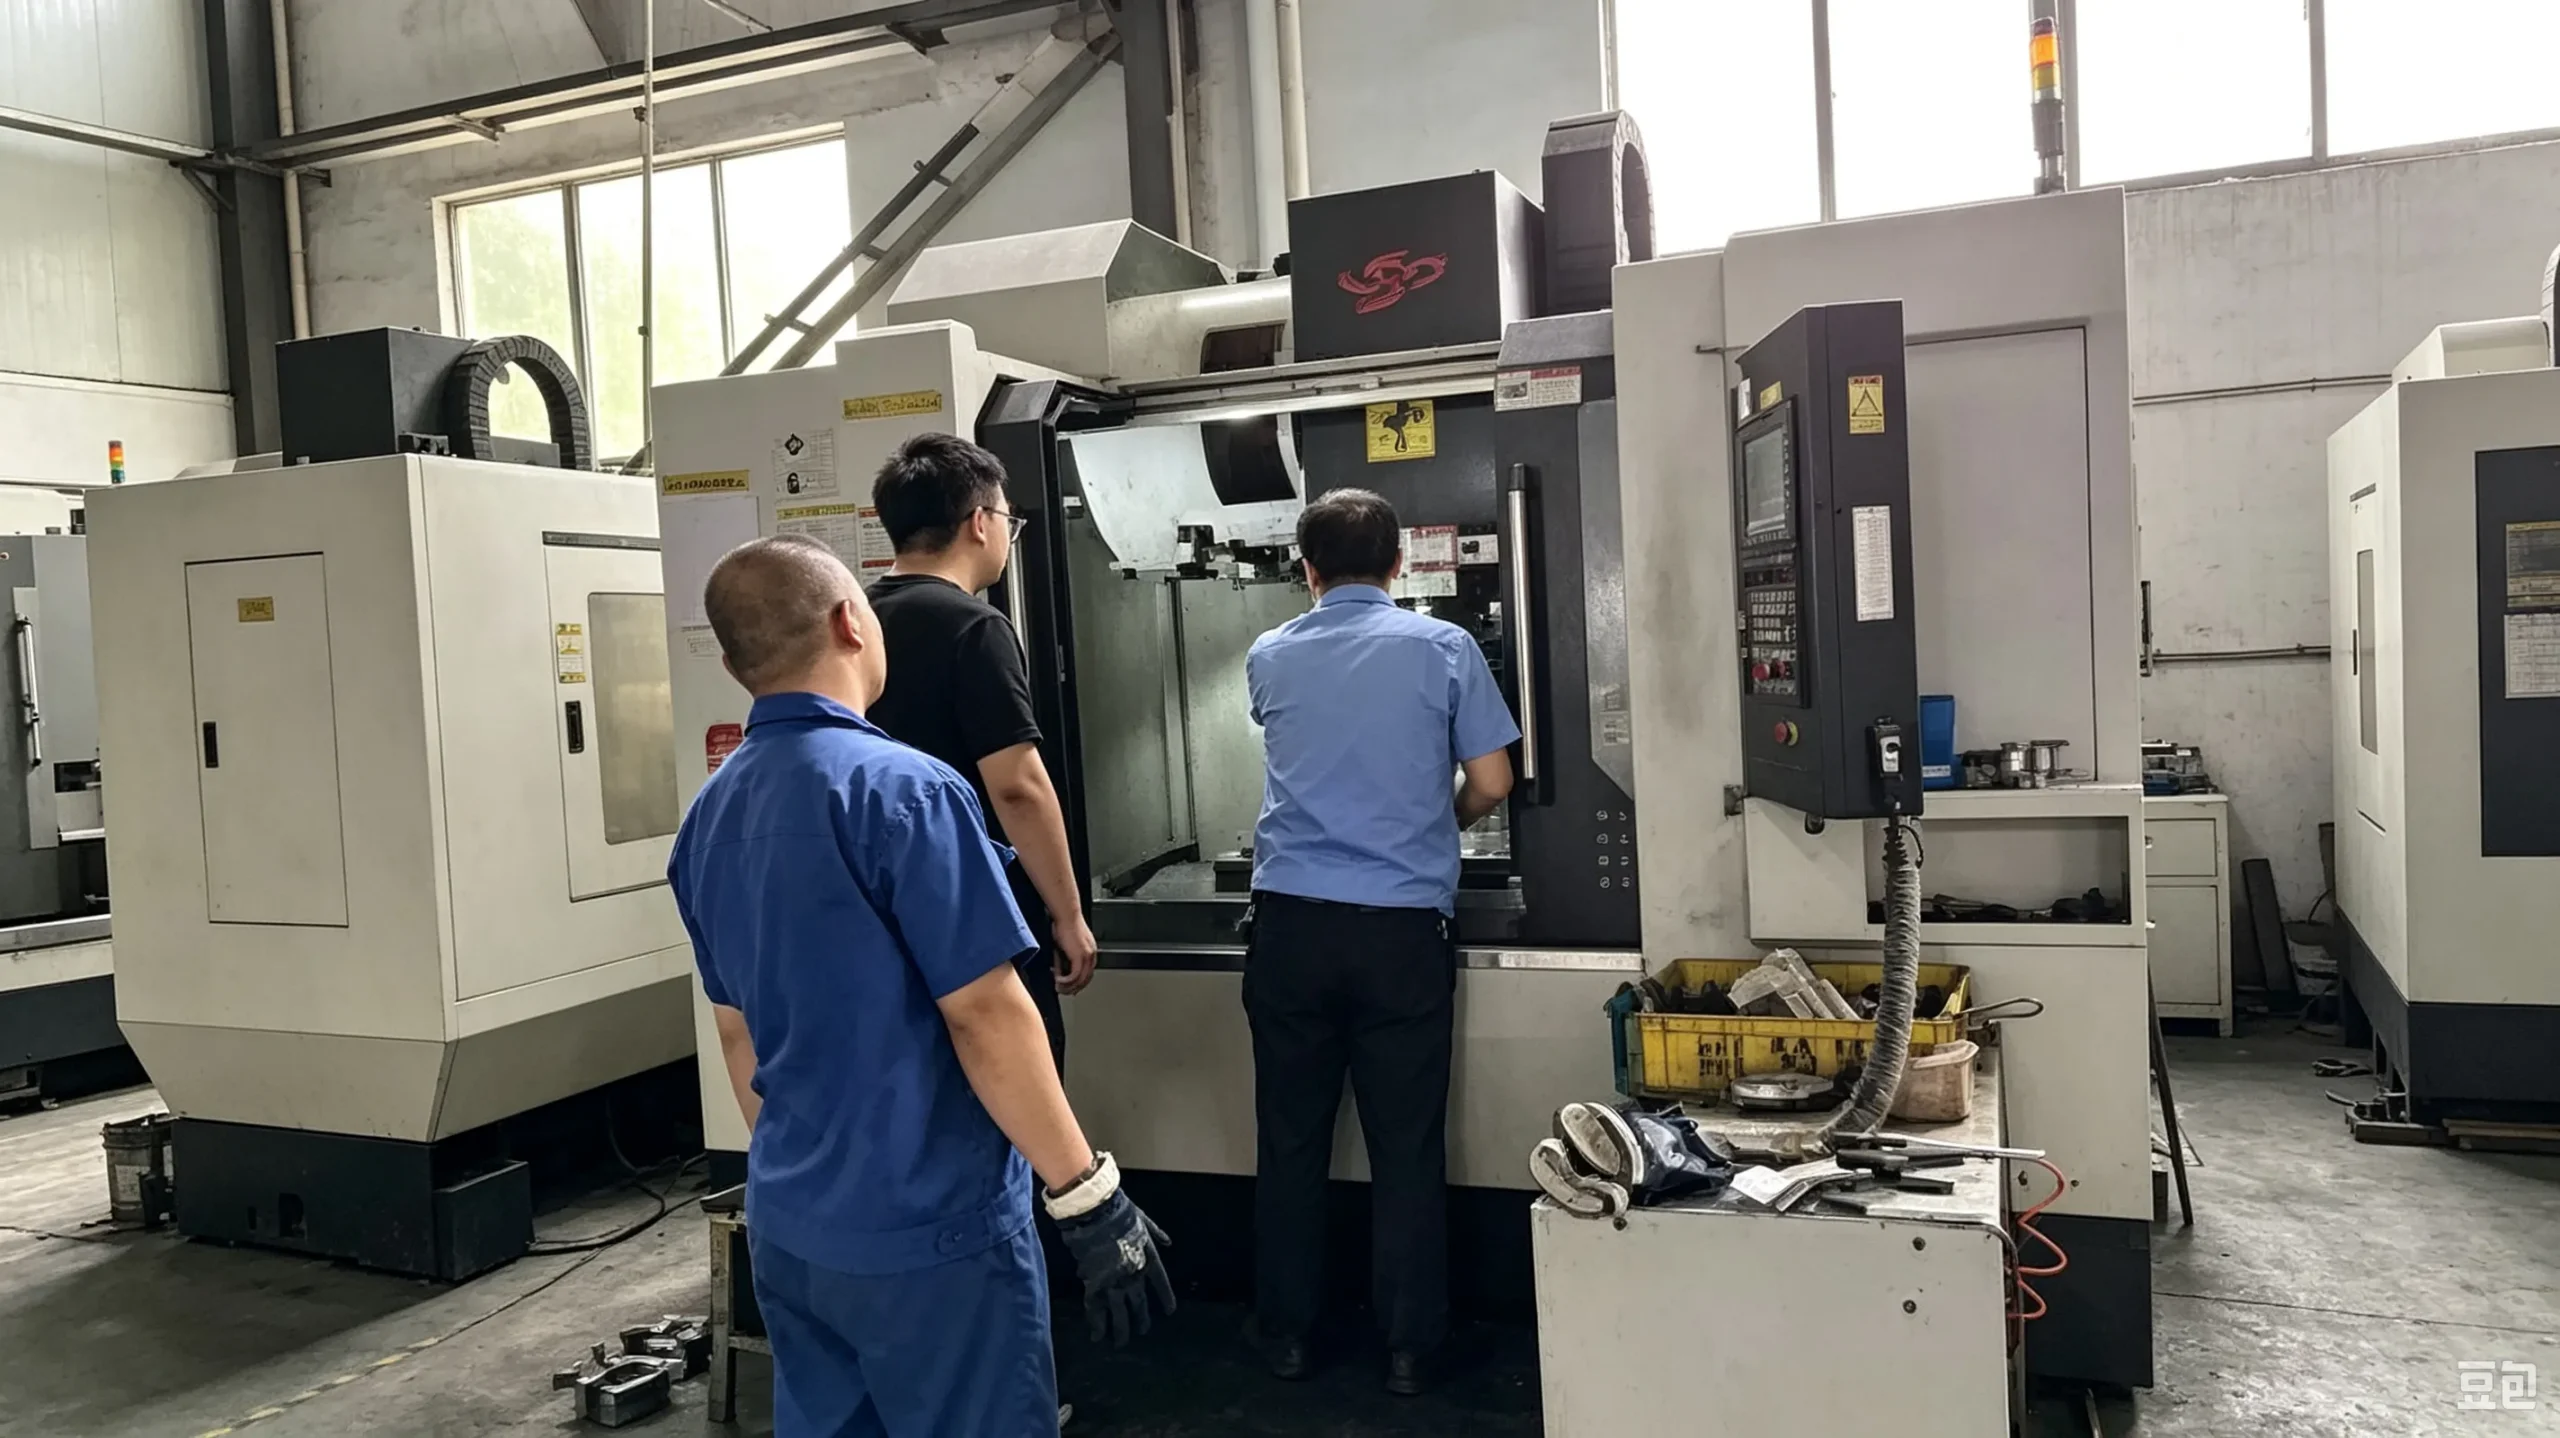
Based at Shenhua Road, Hangzhou, China, our manufacturing operation supplies processed meat equipment to customers across more than 60 countries. Every machine that leaves our facility has been run-tested at rated output before shipping — not just electrical-tested. For vacuum fillers, that means 4-hour sustained operation at full throughput with documented vacuum stability logs provided to the customer.
20+ Years Manufacturing
Decades of specialized experience in sausage processing equipment for global meat industries.
60+ Countries Served
Active installations across Europe, Southeast Asia, North America, and South America.
Full Line Integration
We supply every station from grinding to hanging — single-source responsibility, matched control architecture.
Certified Quality
CE and ISO-compliant manufacturing with full run-test documentation shipped with every machine.
Maintenance Practices That Protect Filling Quality Over Time
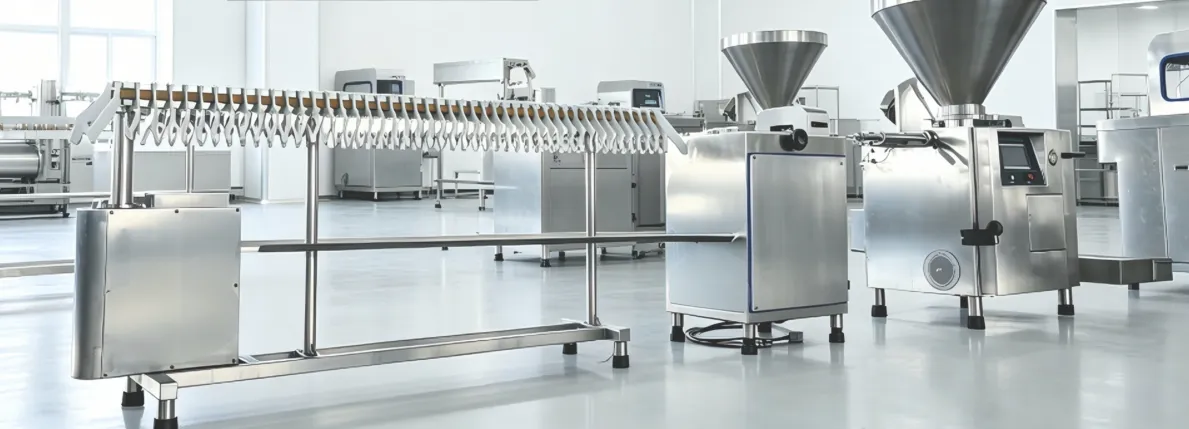
A vane-type vacuum filler that ran perfectly at commissioning will degrade over time without a structured maintenance schedule. The three components most responsible for vacuum integrity and air-pocket performance are the vane seals, the vacuum pump membrane, and the fill-chamber O-rings. Wear in any of these doesn’t produce immediate catastrophic failure — it produces gradual vacuum depth reduction that manifests as intermittent air pockets that are hard to diagnose without instrumentation.
Daily and Weekly Checks
Before each production run, verify vacuum gauge reading at idle with the hopper sealed and empty. A reading more than 0.005 MPa lower than the baseline recorded at commissioning indicates seal wear that warrants investigation before the shift begins. Weekly, disassemble the nozzle assembly and inspect O-ring contact surfaces for scoring or embedded meat particle residue — both reduce sealing efficiency and create void-nucleation sites during operation.
Vane Replacement Intervals
Vane wear is the primary driver of throughput reduction and air pocket recurrence in high-cycle vacuum sausage fillers. At 6,500 kg/h continuous operation, vanes should be inspected at 2,000-hour intervals and replaced at 3,500 hours or when clearance exceeds the manufacturer’s tolerance — whichever comes first. Running beyond this interval to avoid downtime typically results in a 12–18% throughput loss and significantly elevated defect rates on collagen casing products specifically. Contact our technical team for the OEM vane specification for your machine model.
Recommended Products for Your Collagen Casing Sausage Line
The equipment below forms the core of a complete, air-pocket-free high-speed sausage filling and hanging line. Each unit is available individually or as a configured line package.
ZKG-6500 Vacuum Filling Machine
6,500 kg/h vane-type filler with dual-stage vacuum system and servo-controlled portioning for collagen casing.
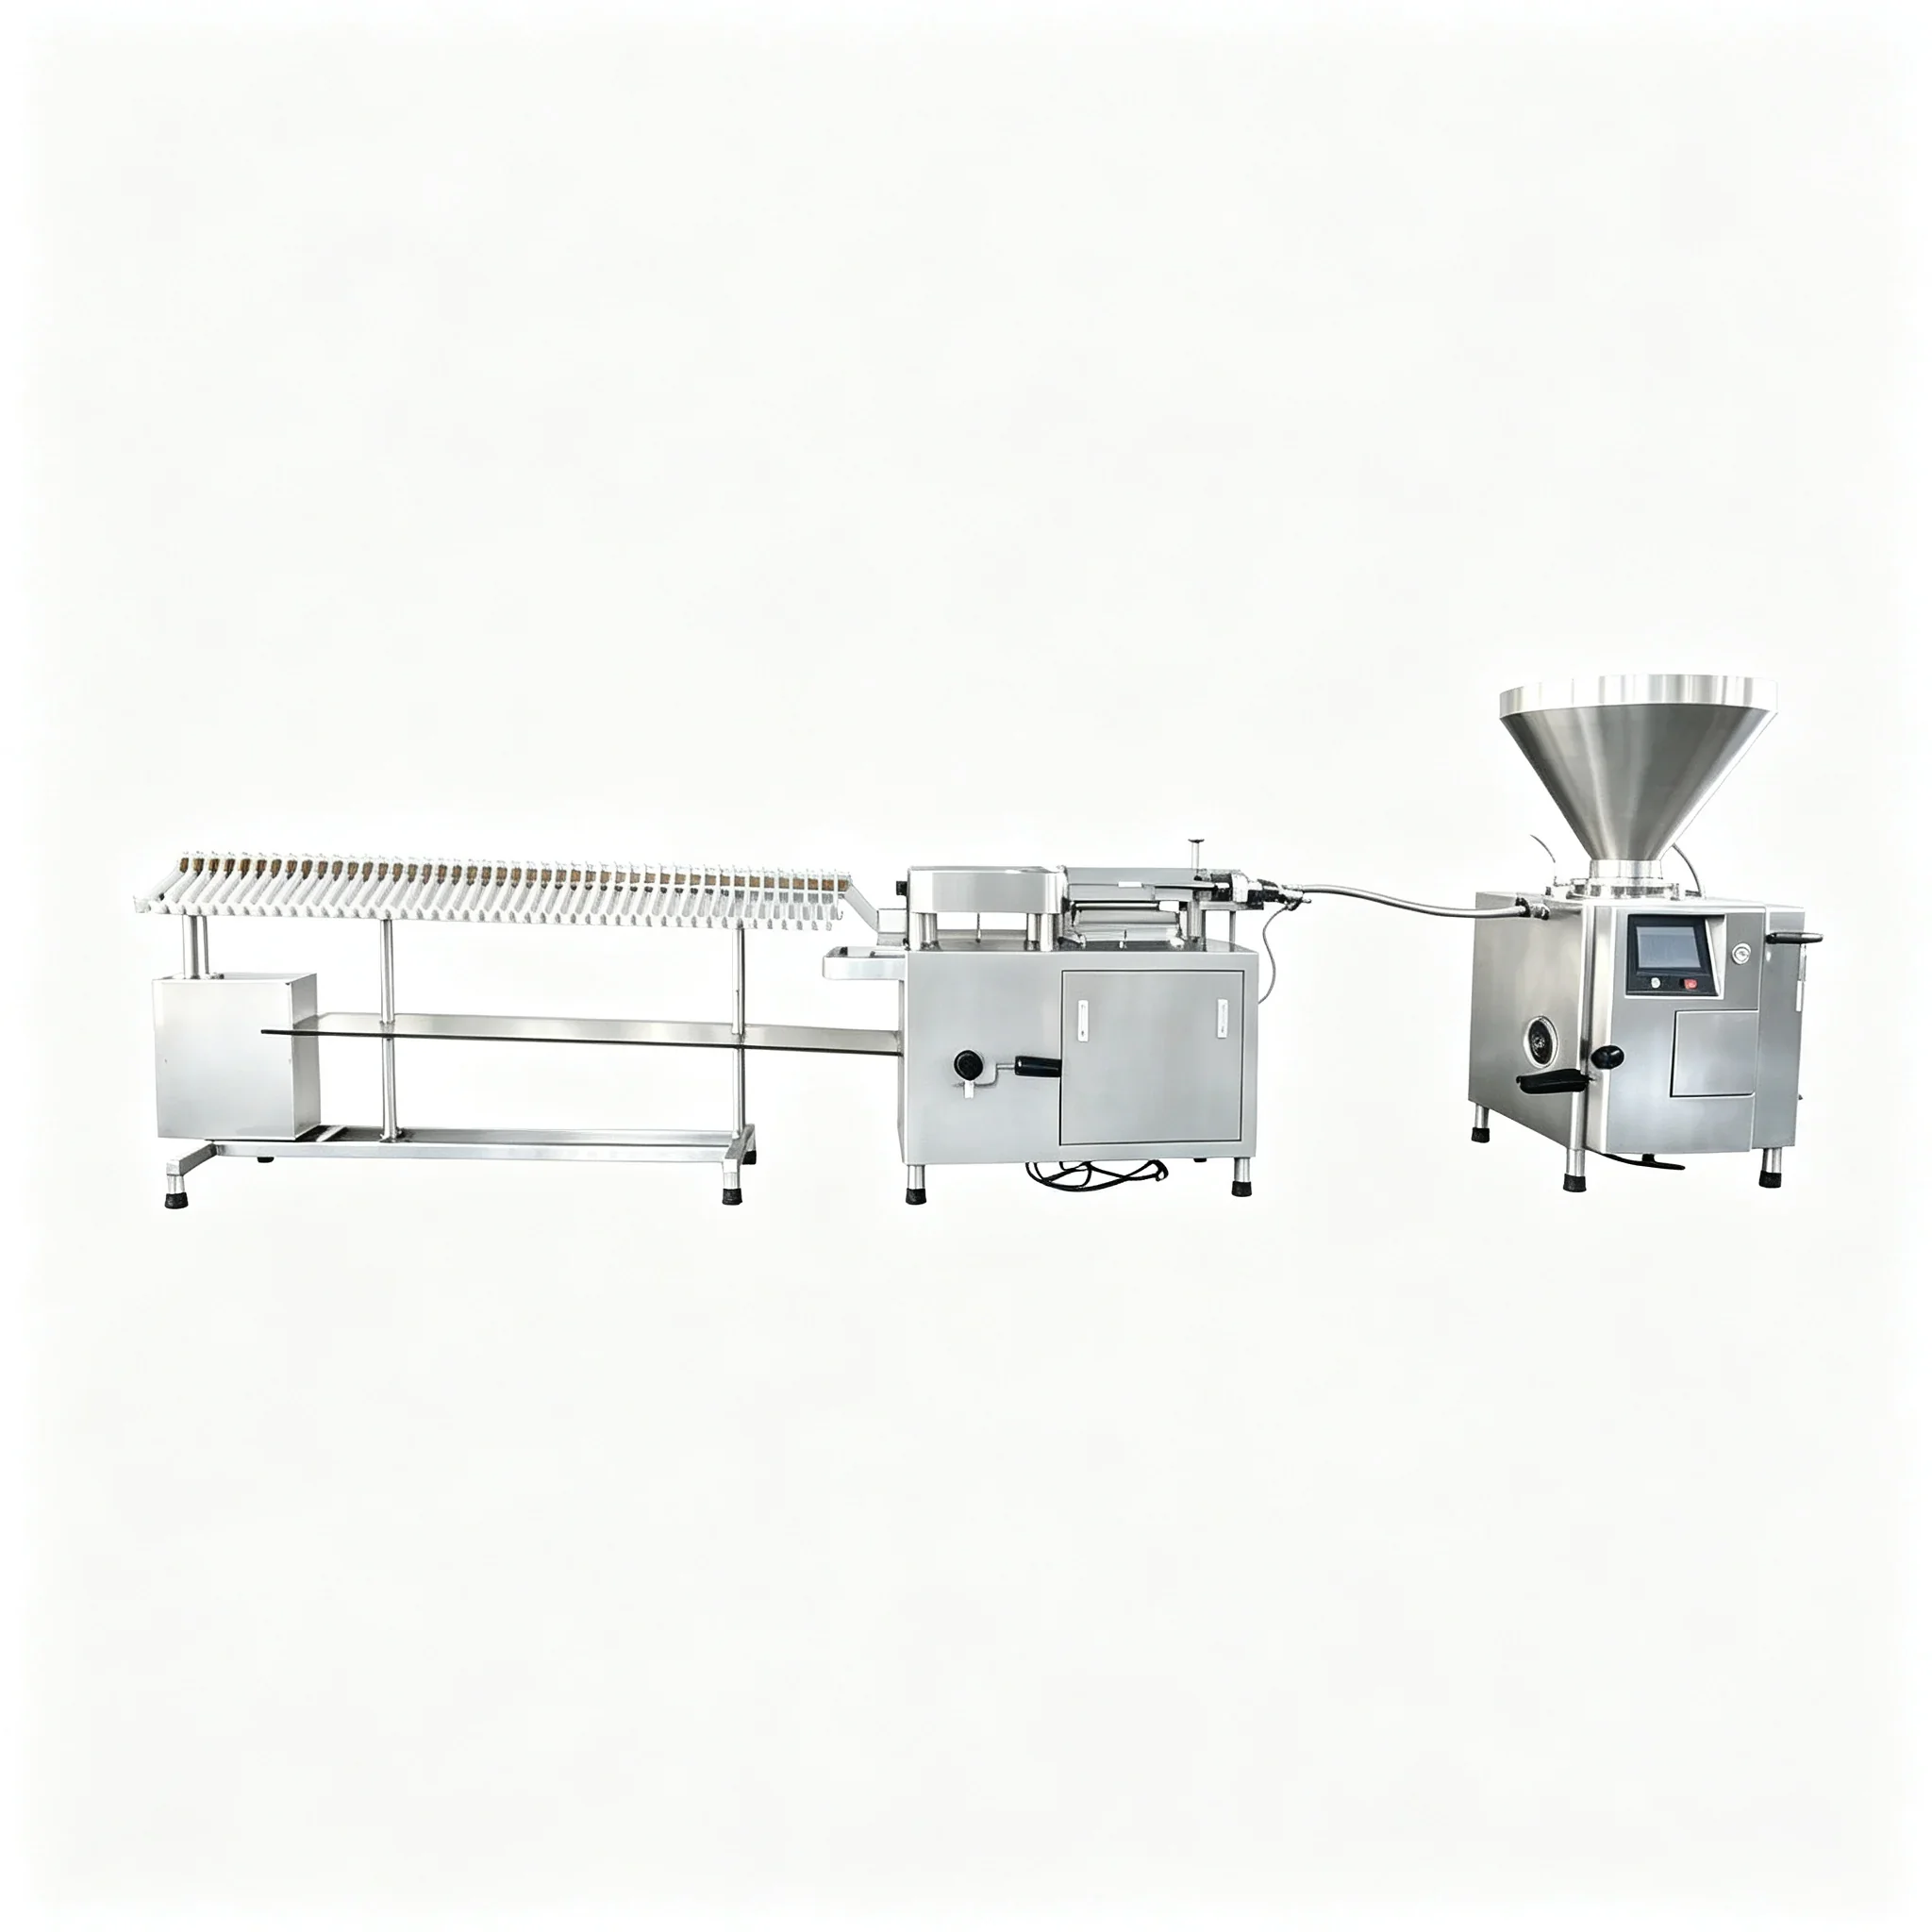
YZG-1200 Auto Linking Hanging Line
Synchronized output for the ZKG-6500 — handles filled casing at rated speed without back-pressure at the stuffing horn.
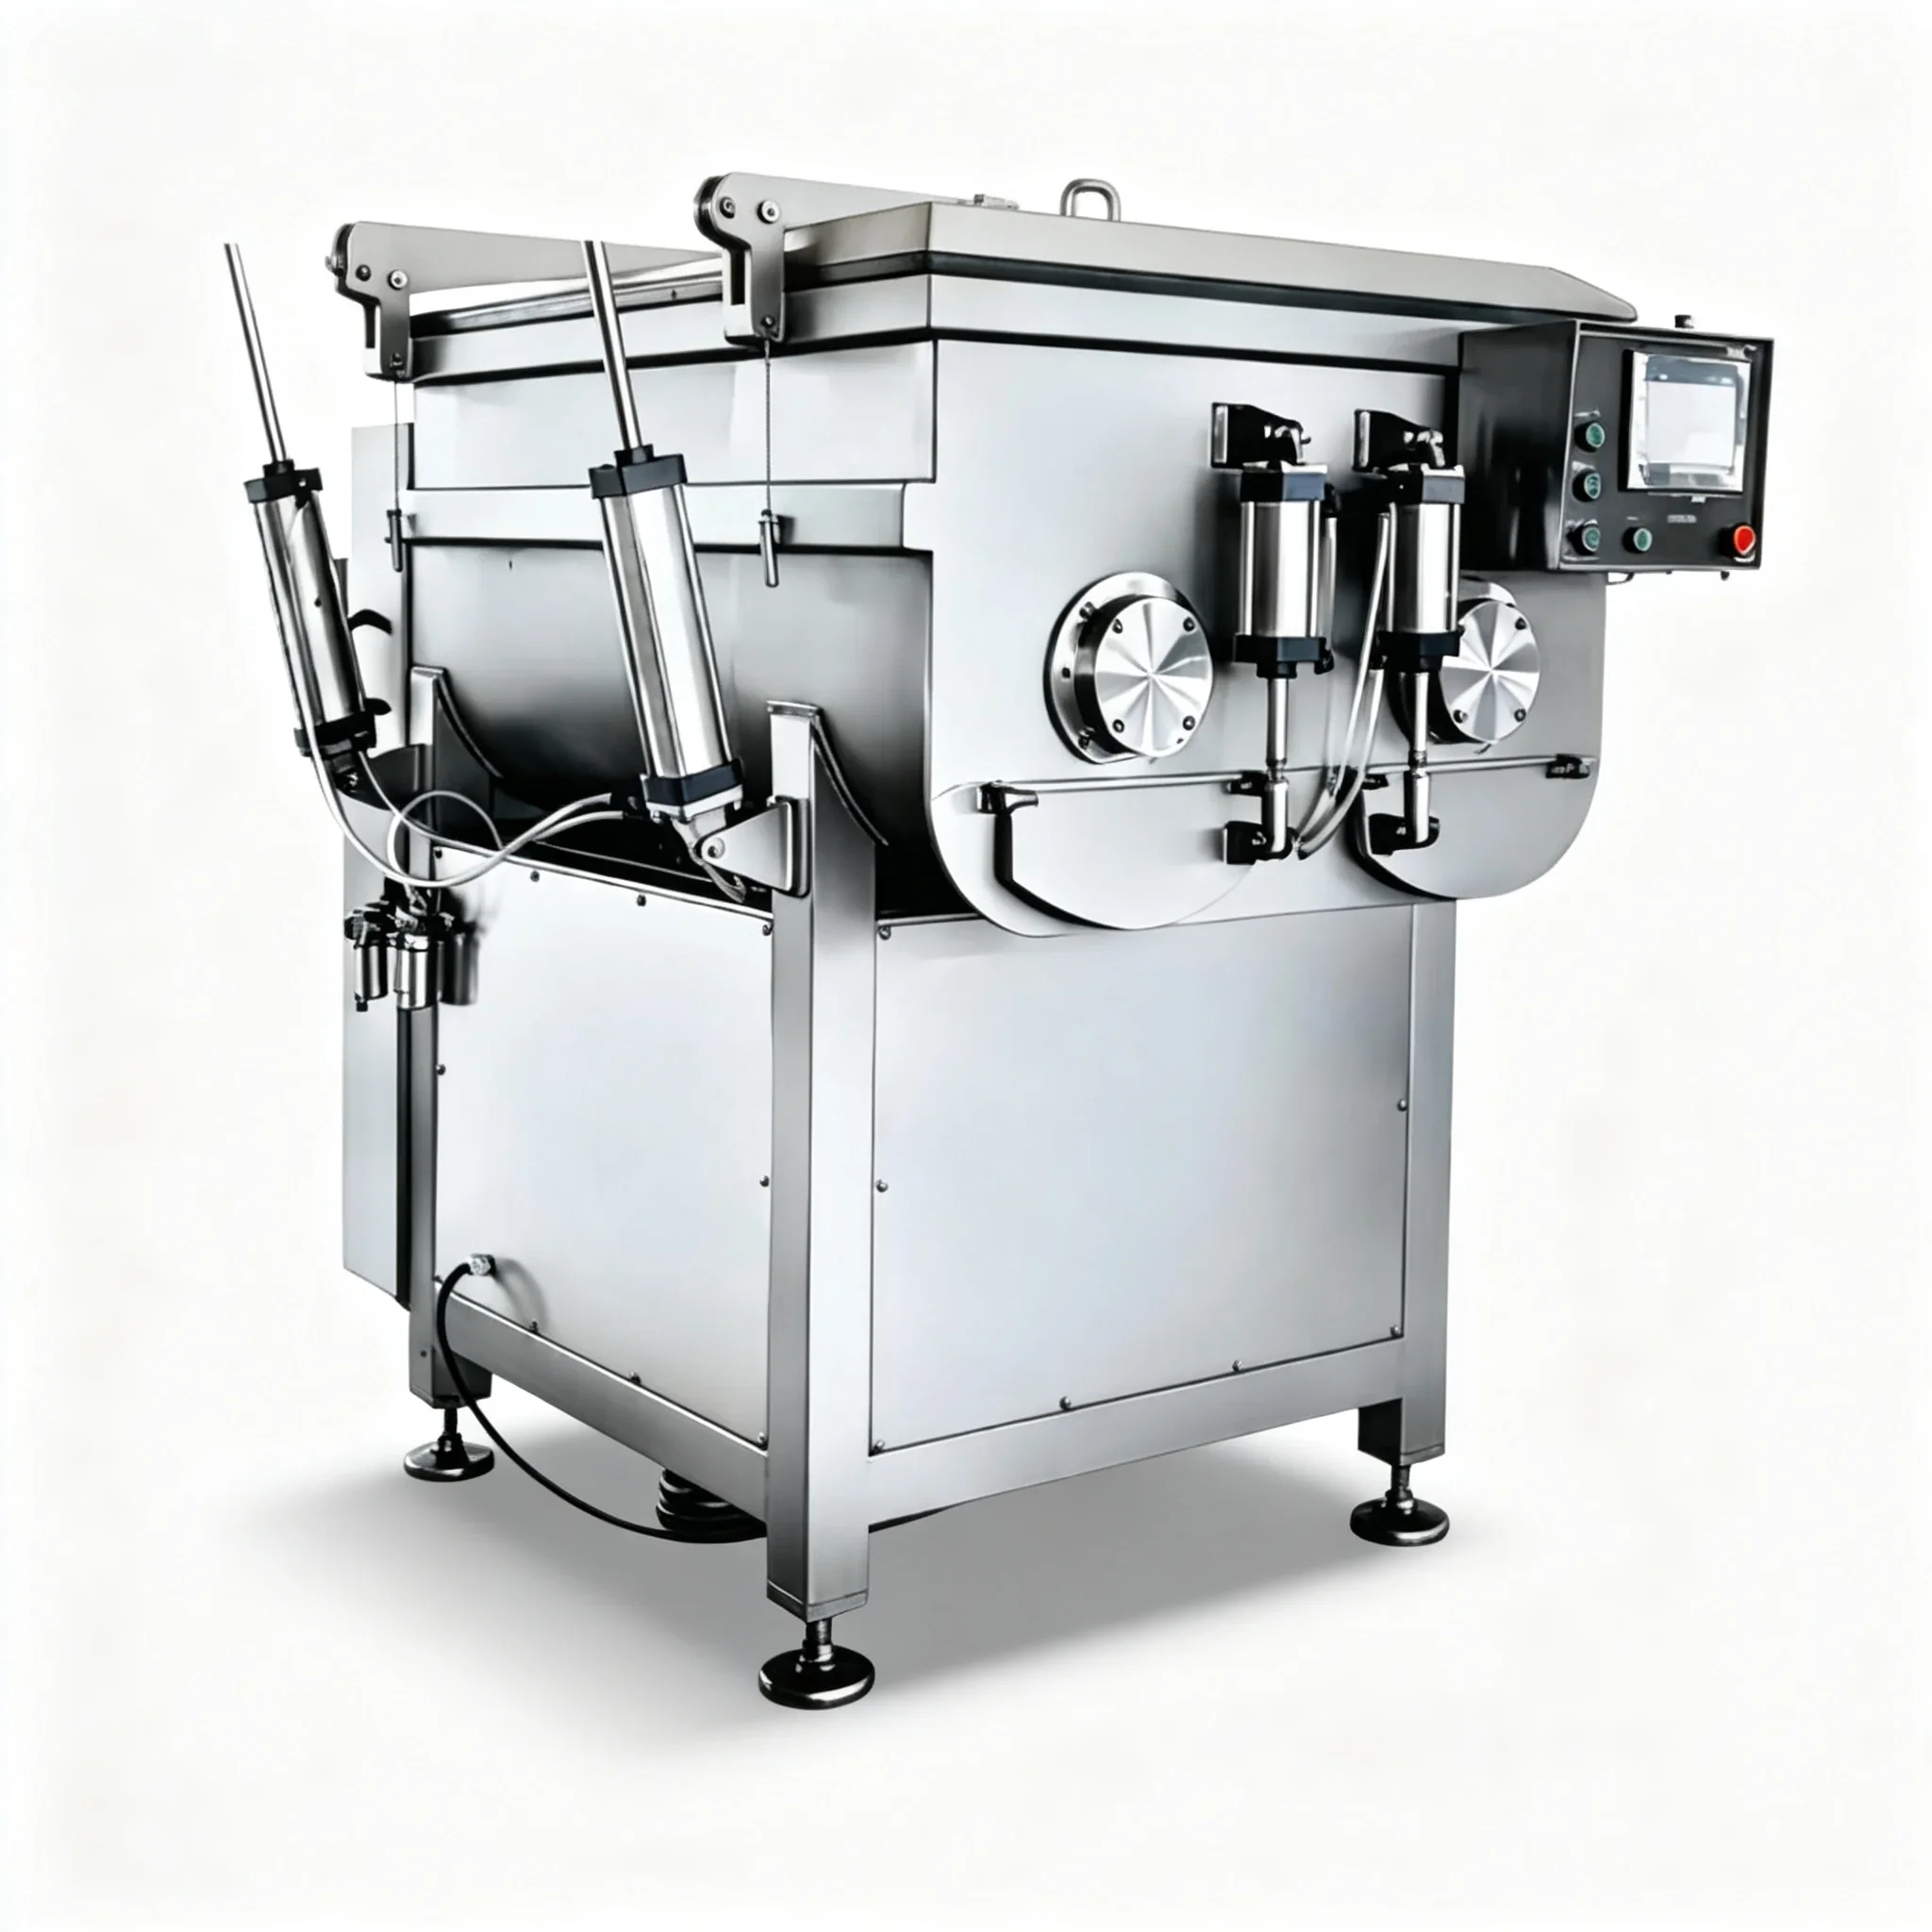
JB-Series Vacuum Mixer
Pre-degasses the meat batch before it enters the hopper — removes dissolved air at source for maximum filling quality.
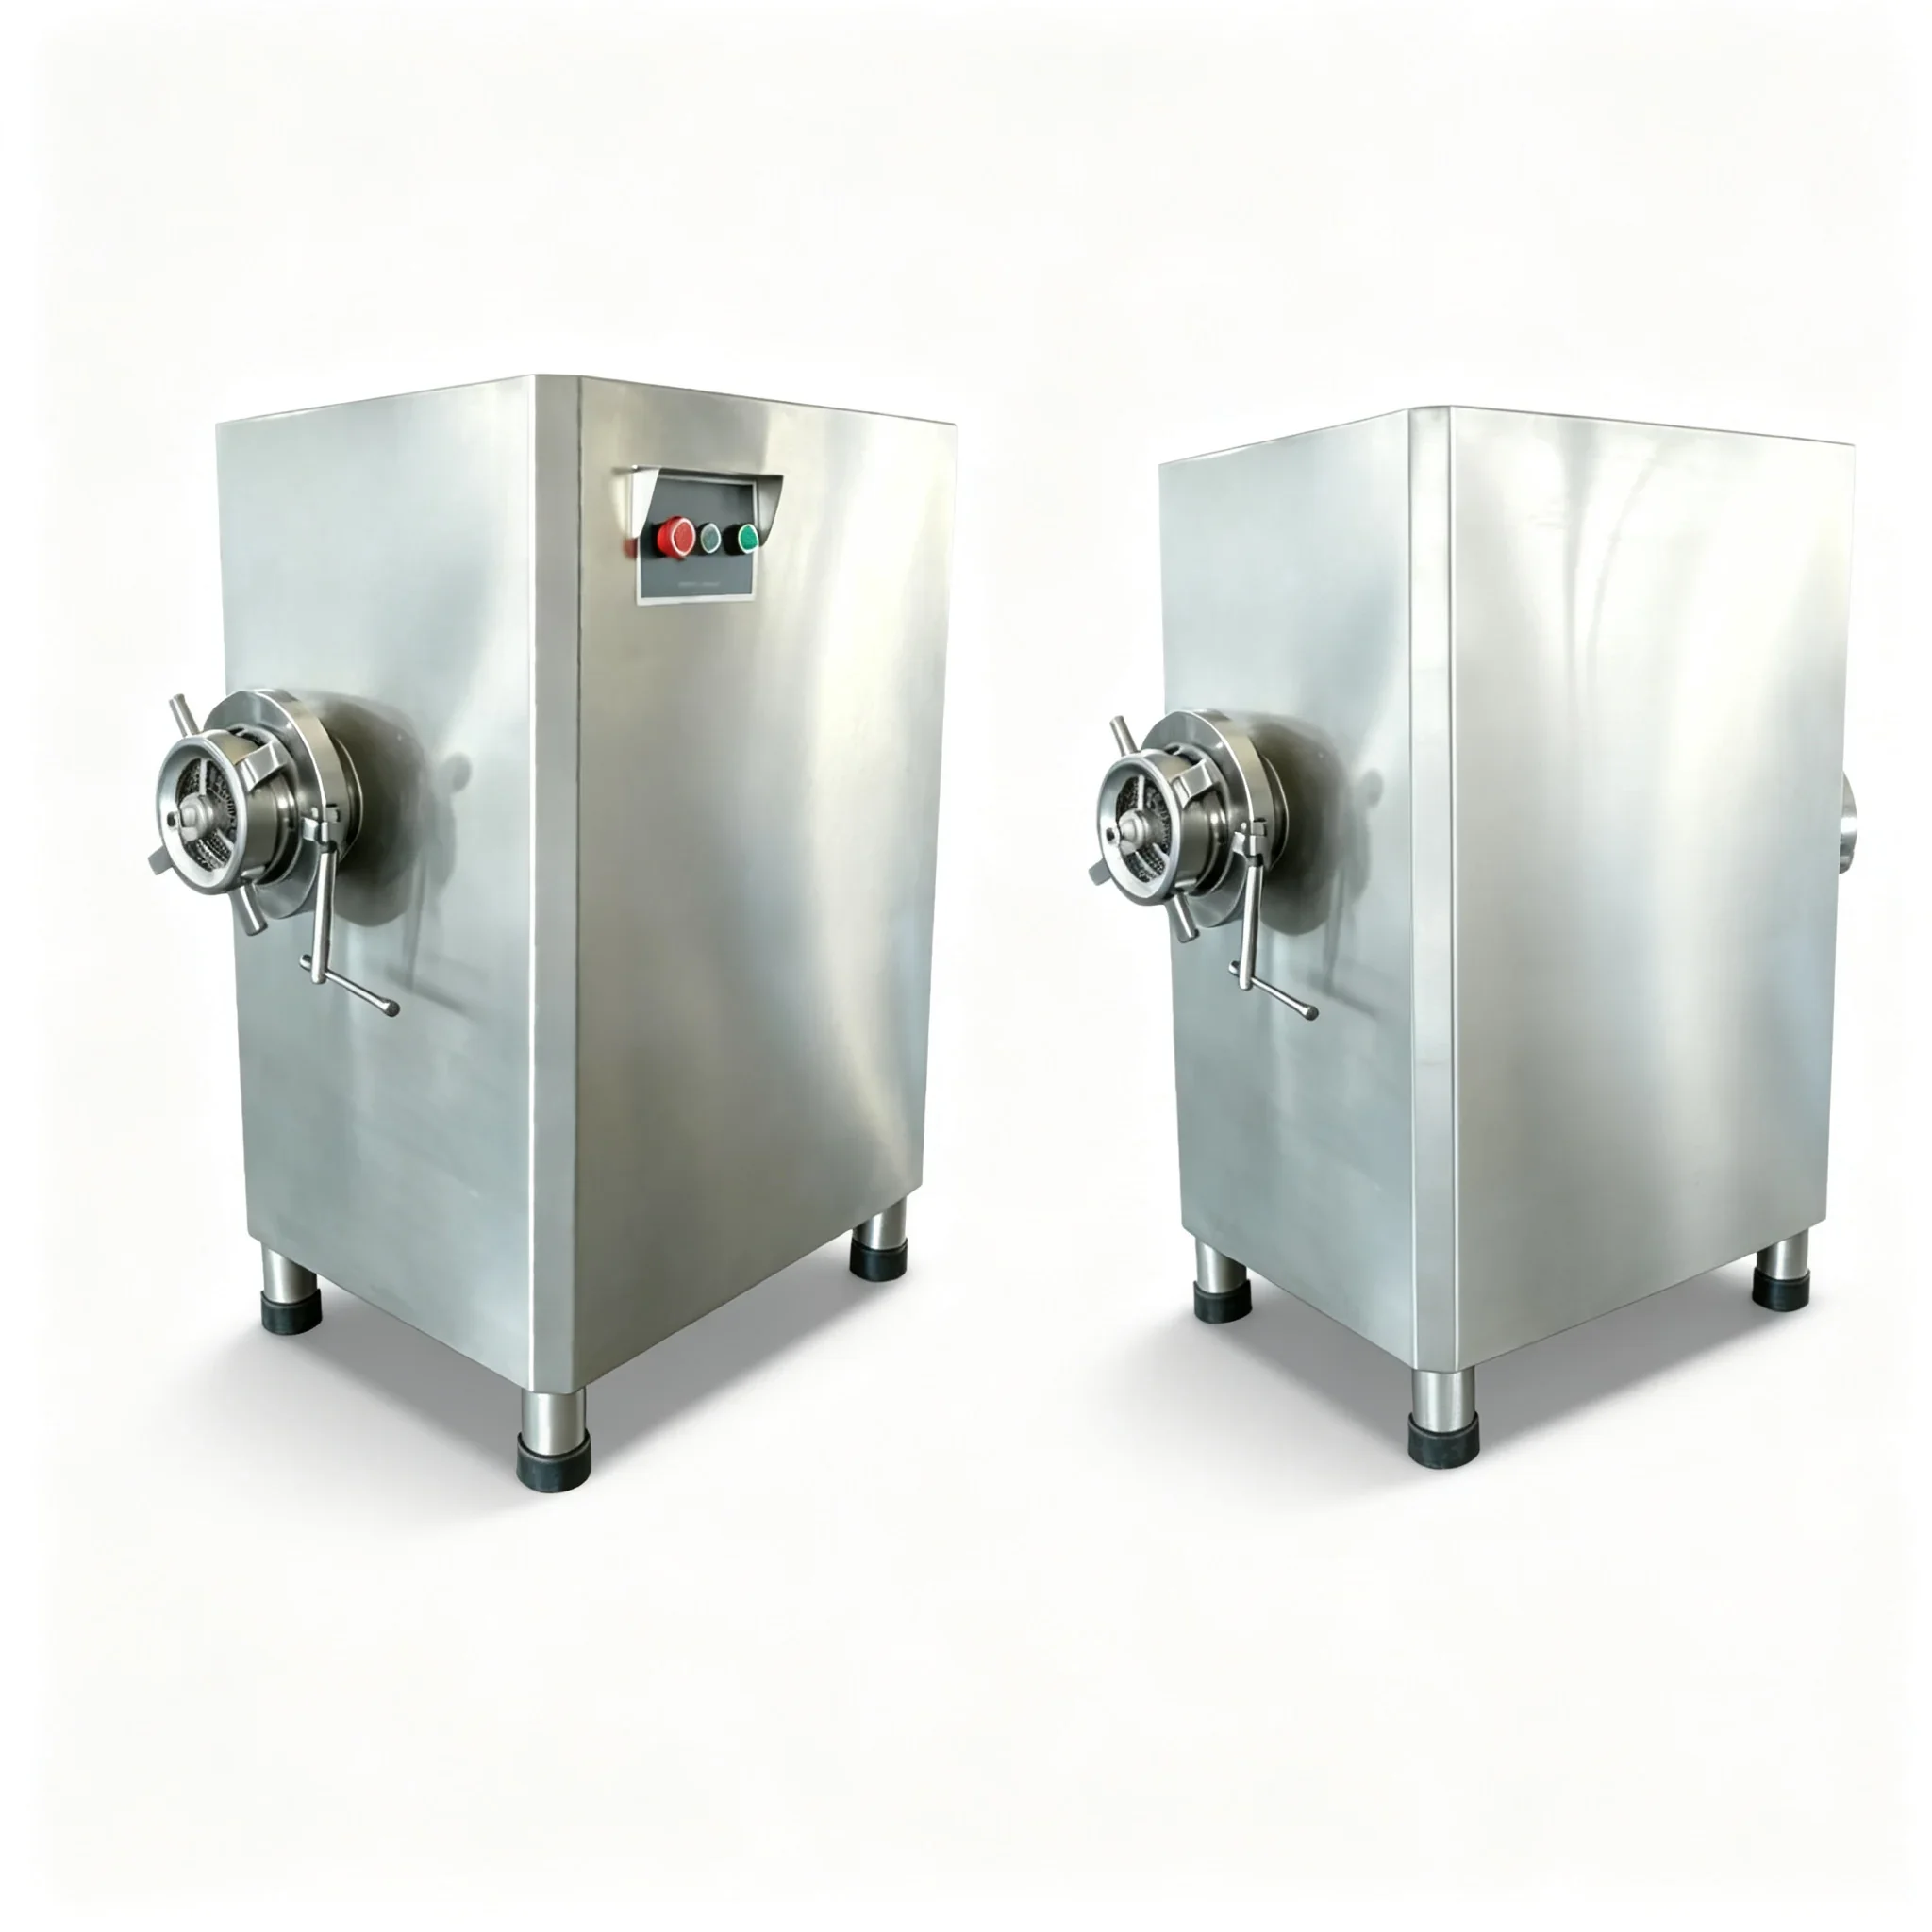
JR-Series Meat Grinder
Handles frozen and fresh block meat with consistent particle sizing — the upstream foundation of uniform paste viscosity.
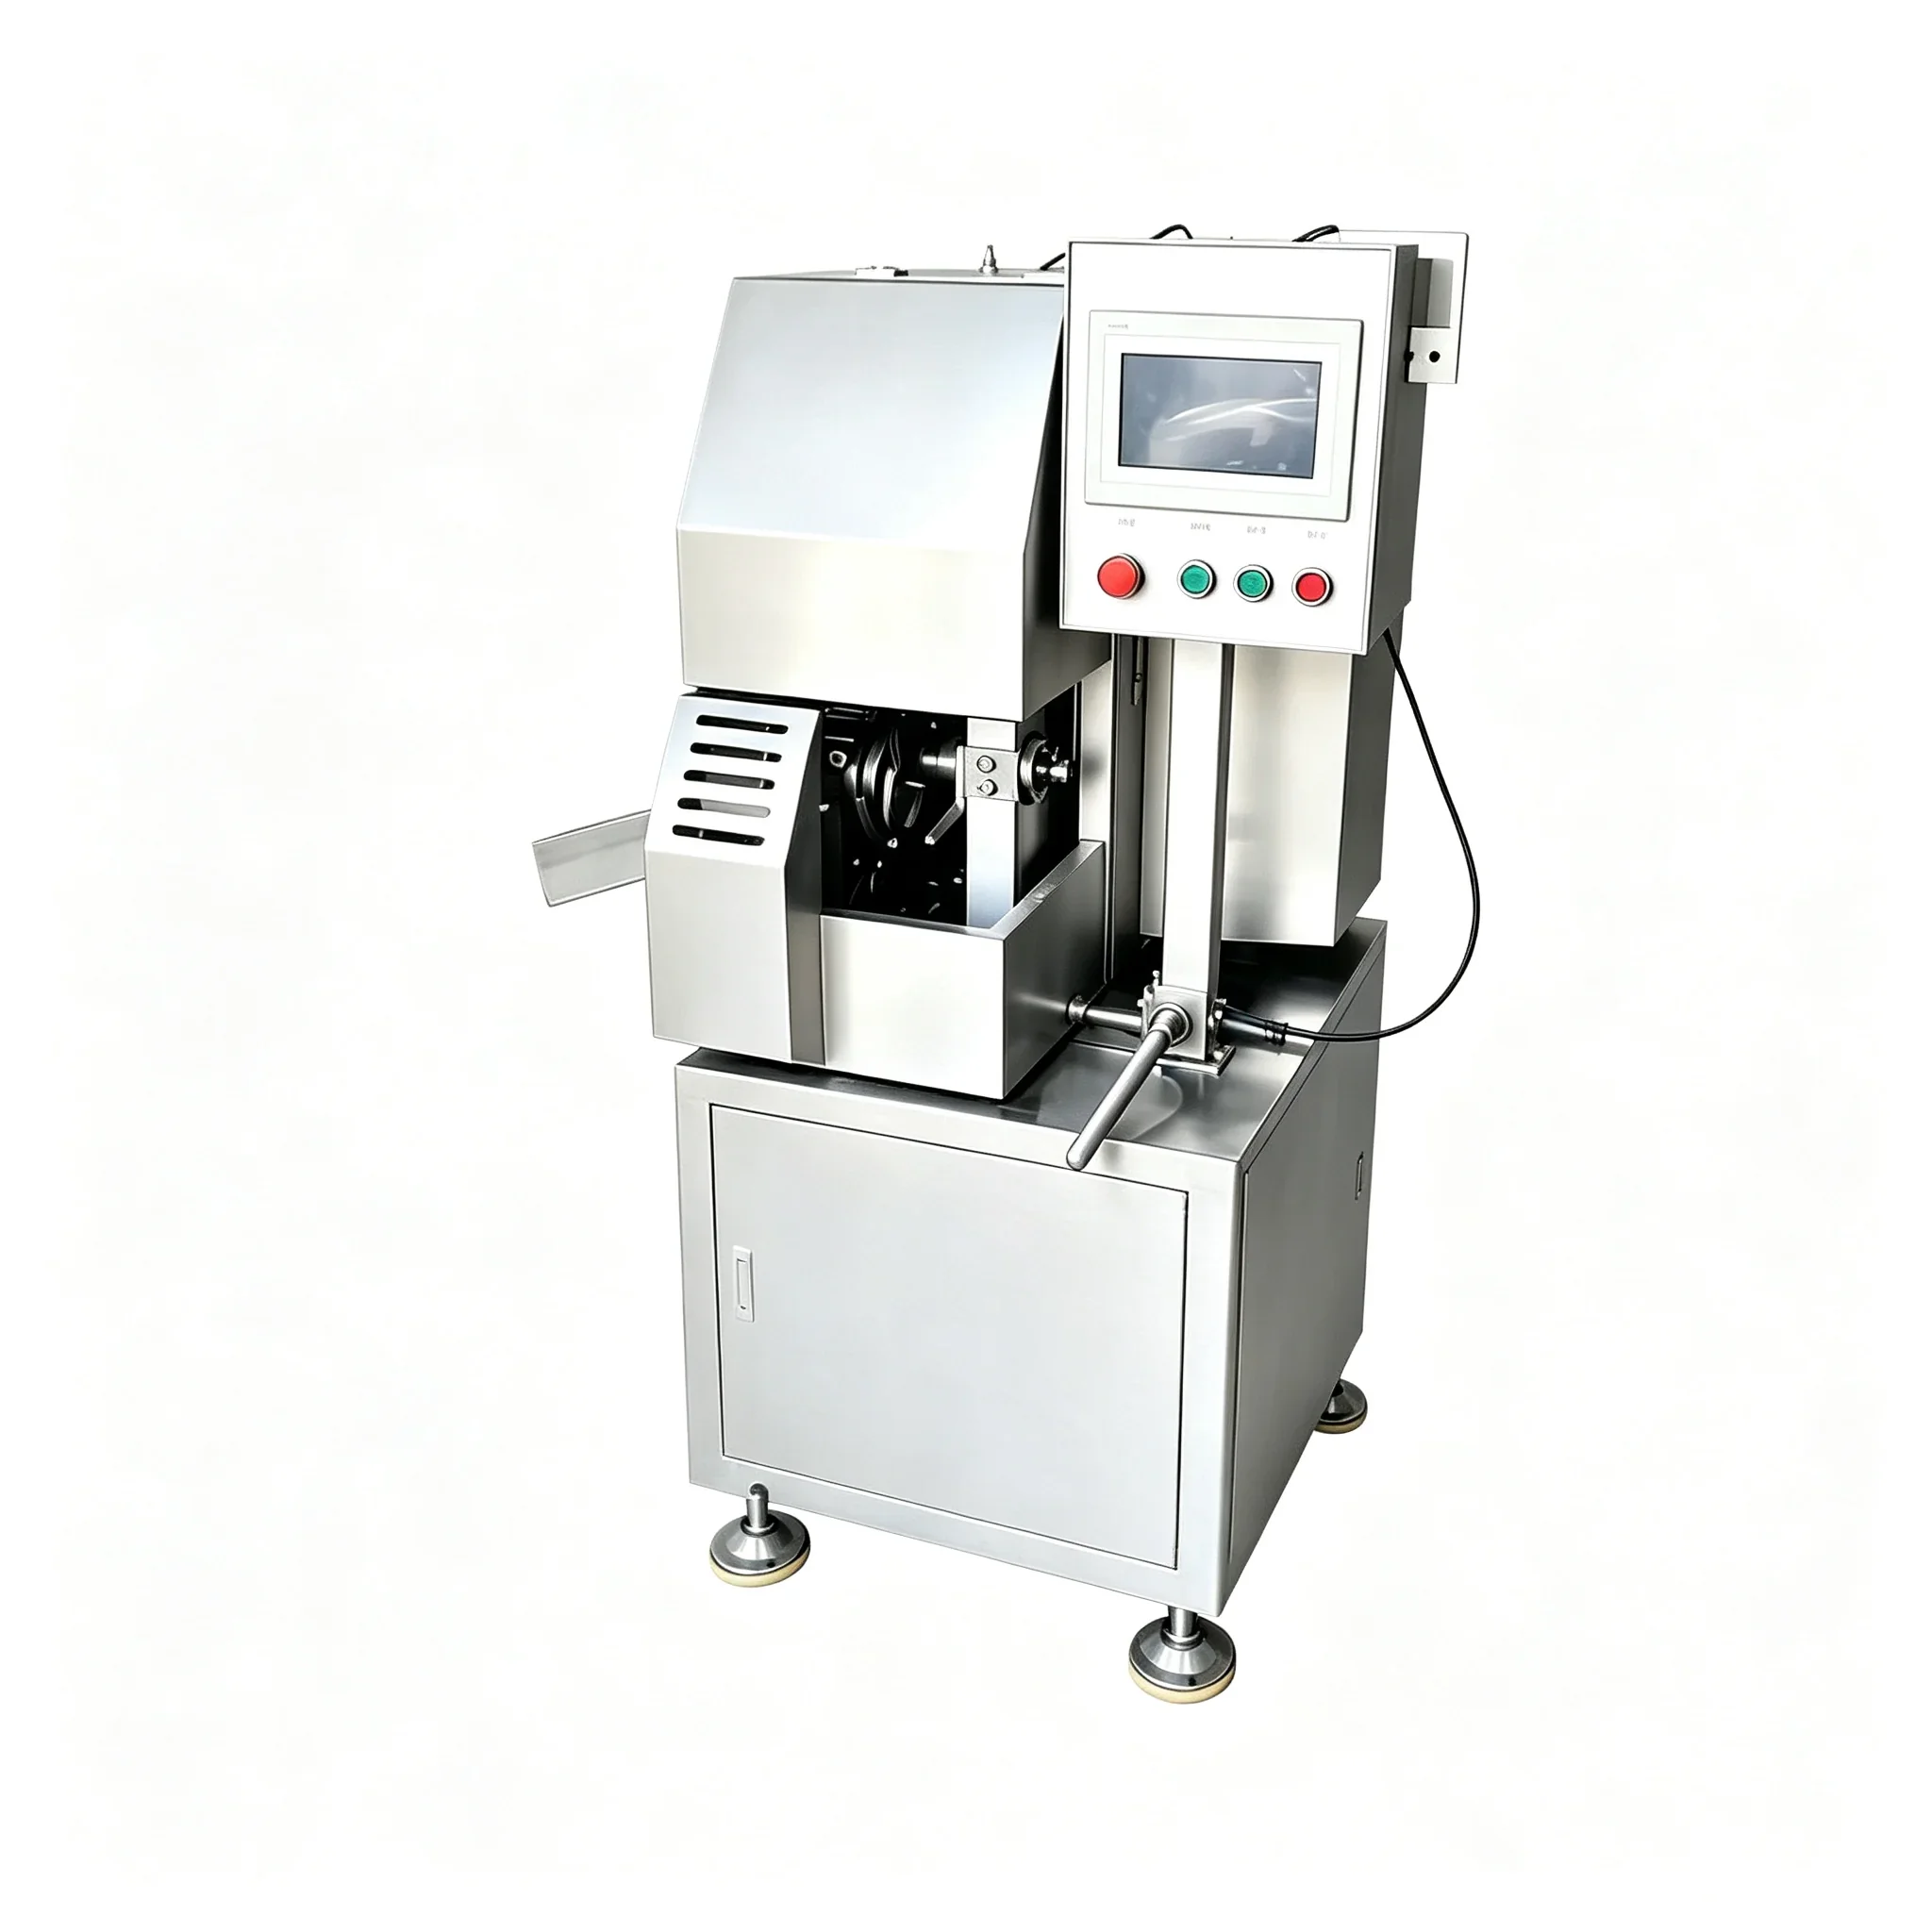
JLSK-II Double Clipping Machine
Seals collagen casing ends at controlled clip tension — prevents fracture-induced air ingress during post-fill handling.
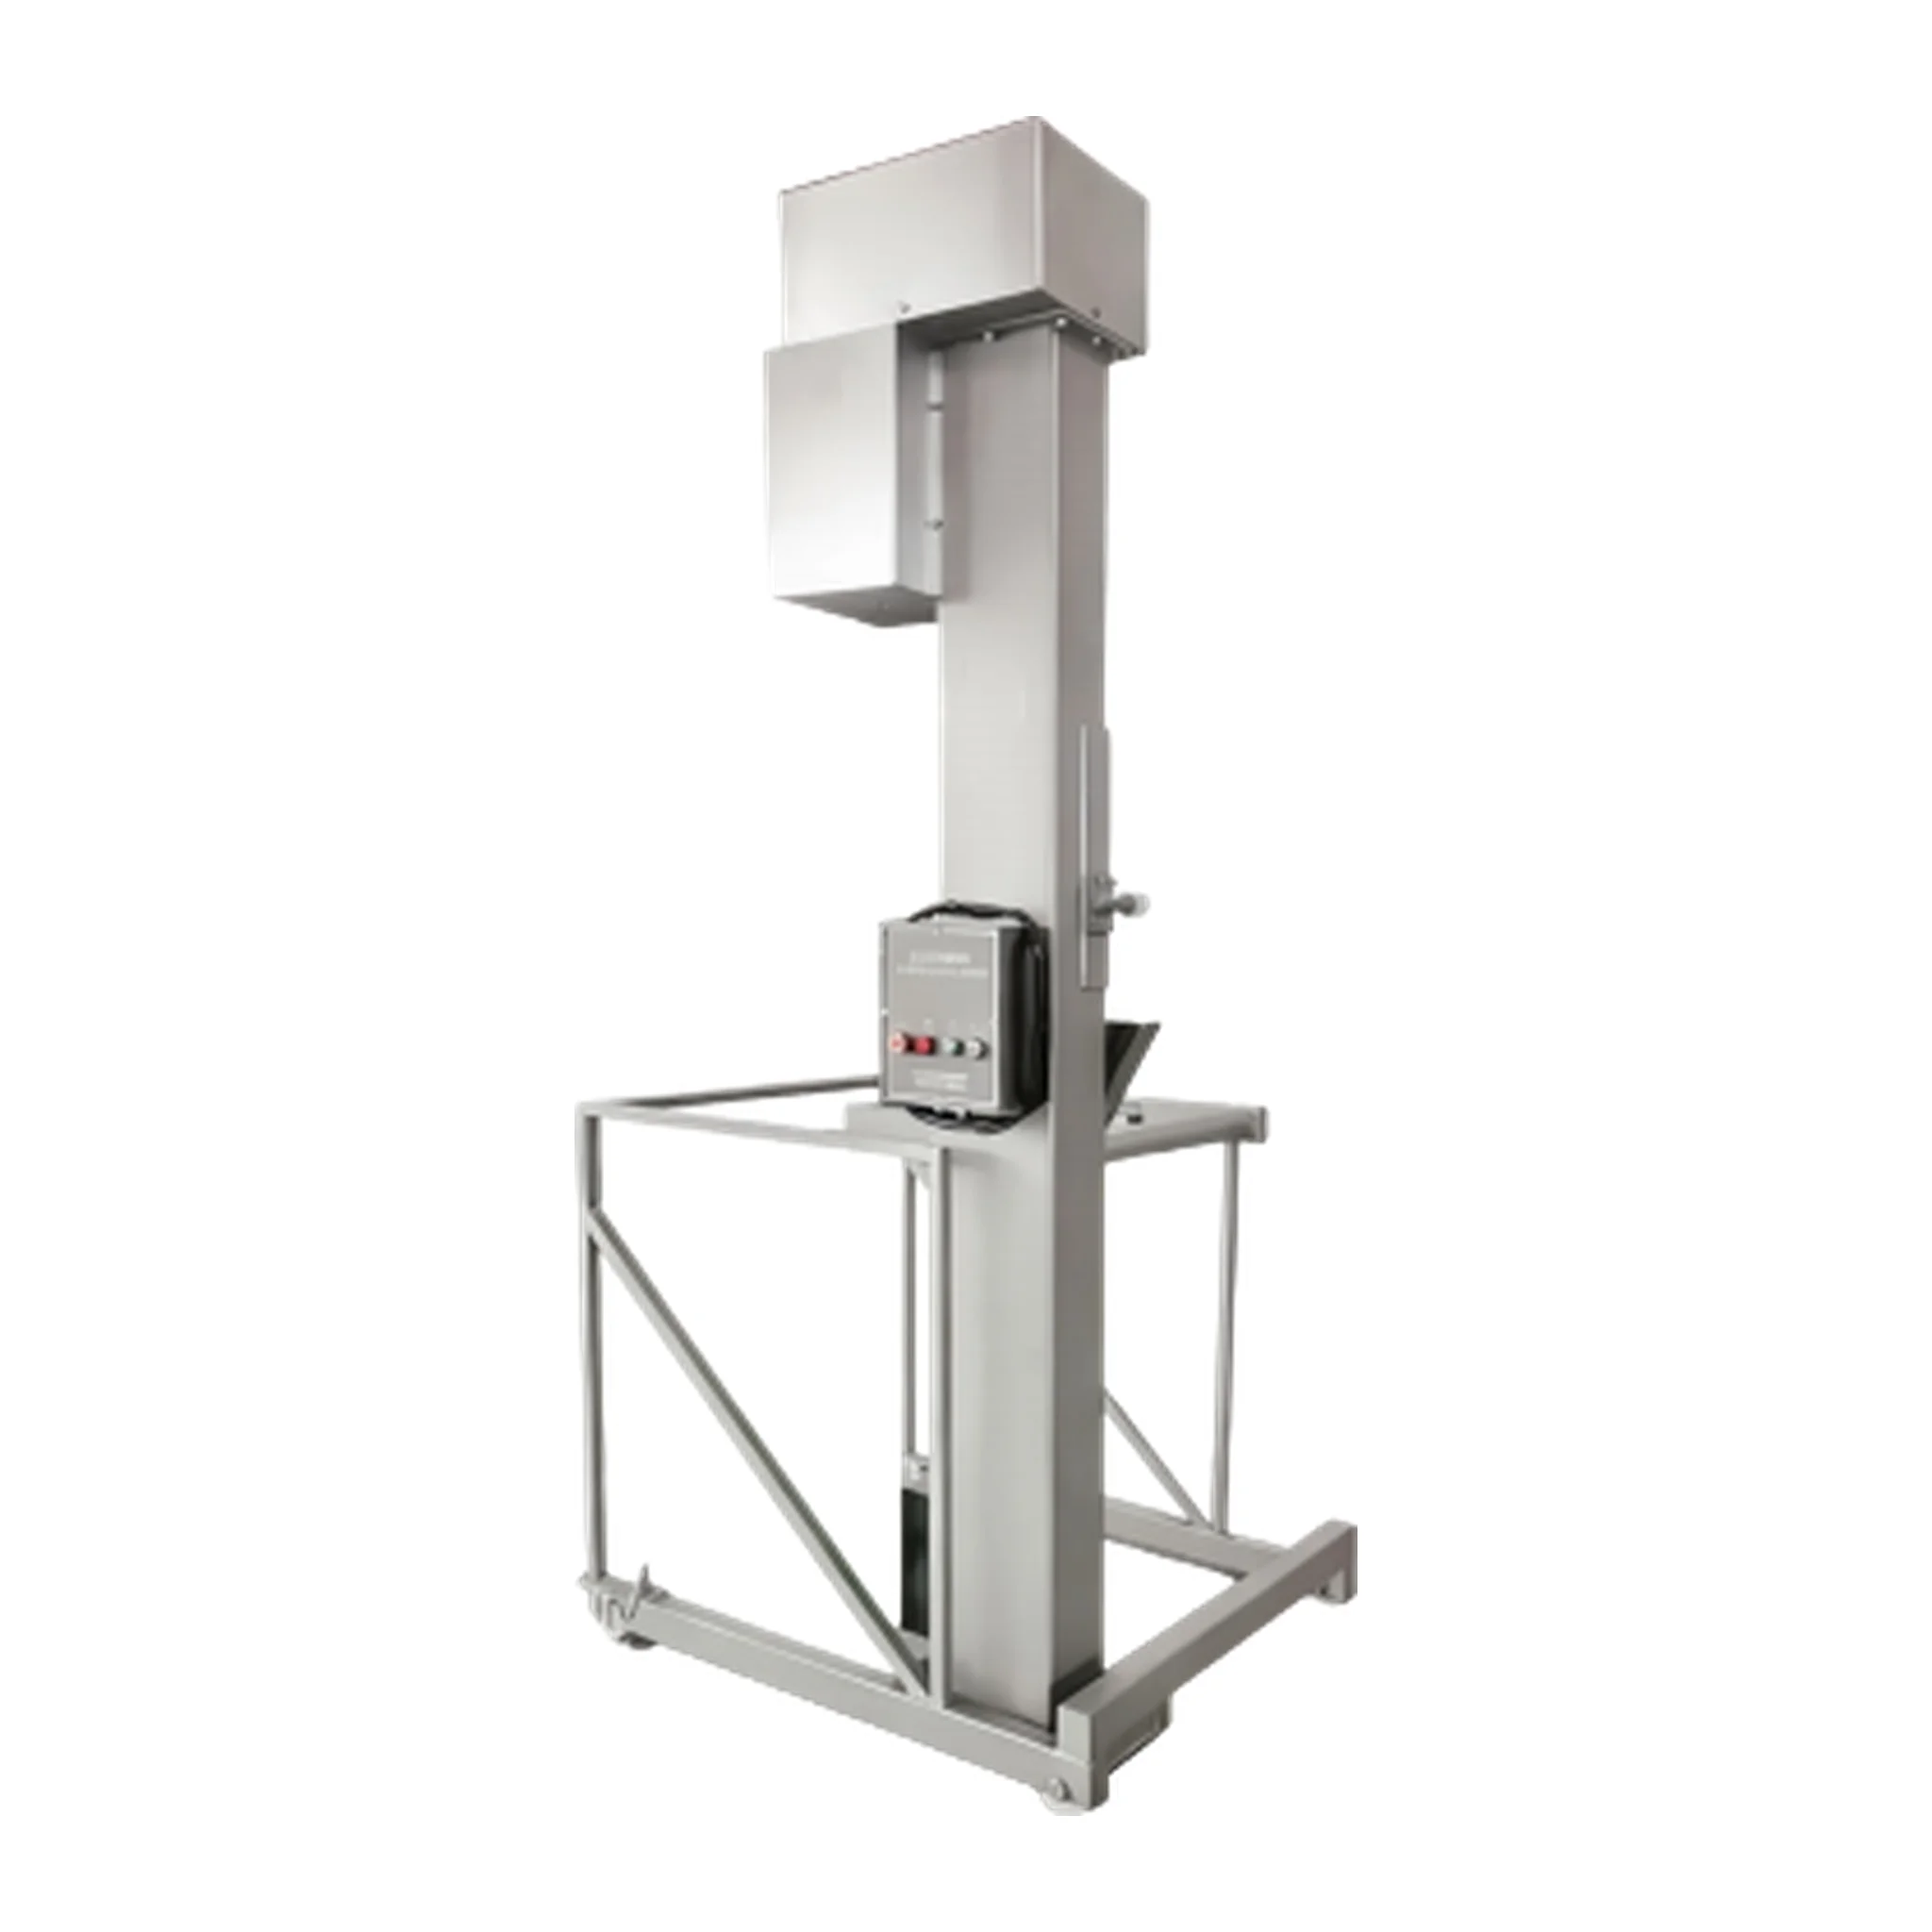
T200 Lifting Machine
Eliminates manual hopper loading gaps — continuous feed into the vacuum filler removes the most preventable source of air pockets.
자주 묻는 질문
가공육장비닷컴 | Shenhua Road, Hangzhou, China 310031