Vacuum fillers and hydraulic sausage stuffers both move meat paste into casing — but the engineering principles behind them produce completely different outcomes at high volume. For frankfurter and hot dog production at industrial scale, choosing the wrong technology costs you in throughput, product consistency, and maintenance downtime. This comparison cuts through marketing claims to show what each machine type actually delivers on a high-volume frankfurter and hot dog line.
The Fundamental Mechanical Difference
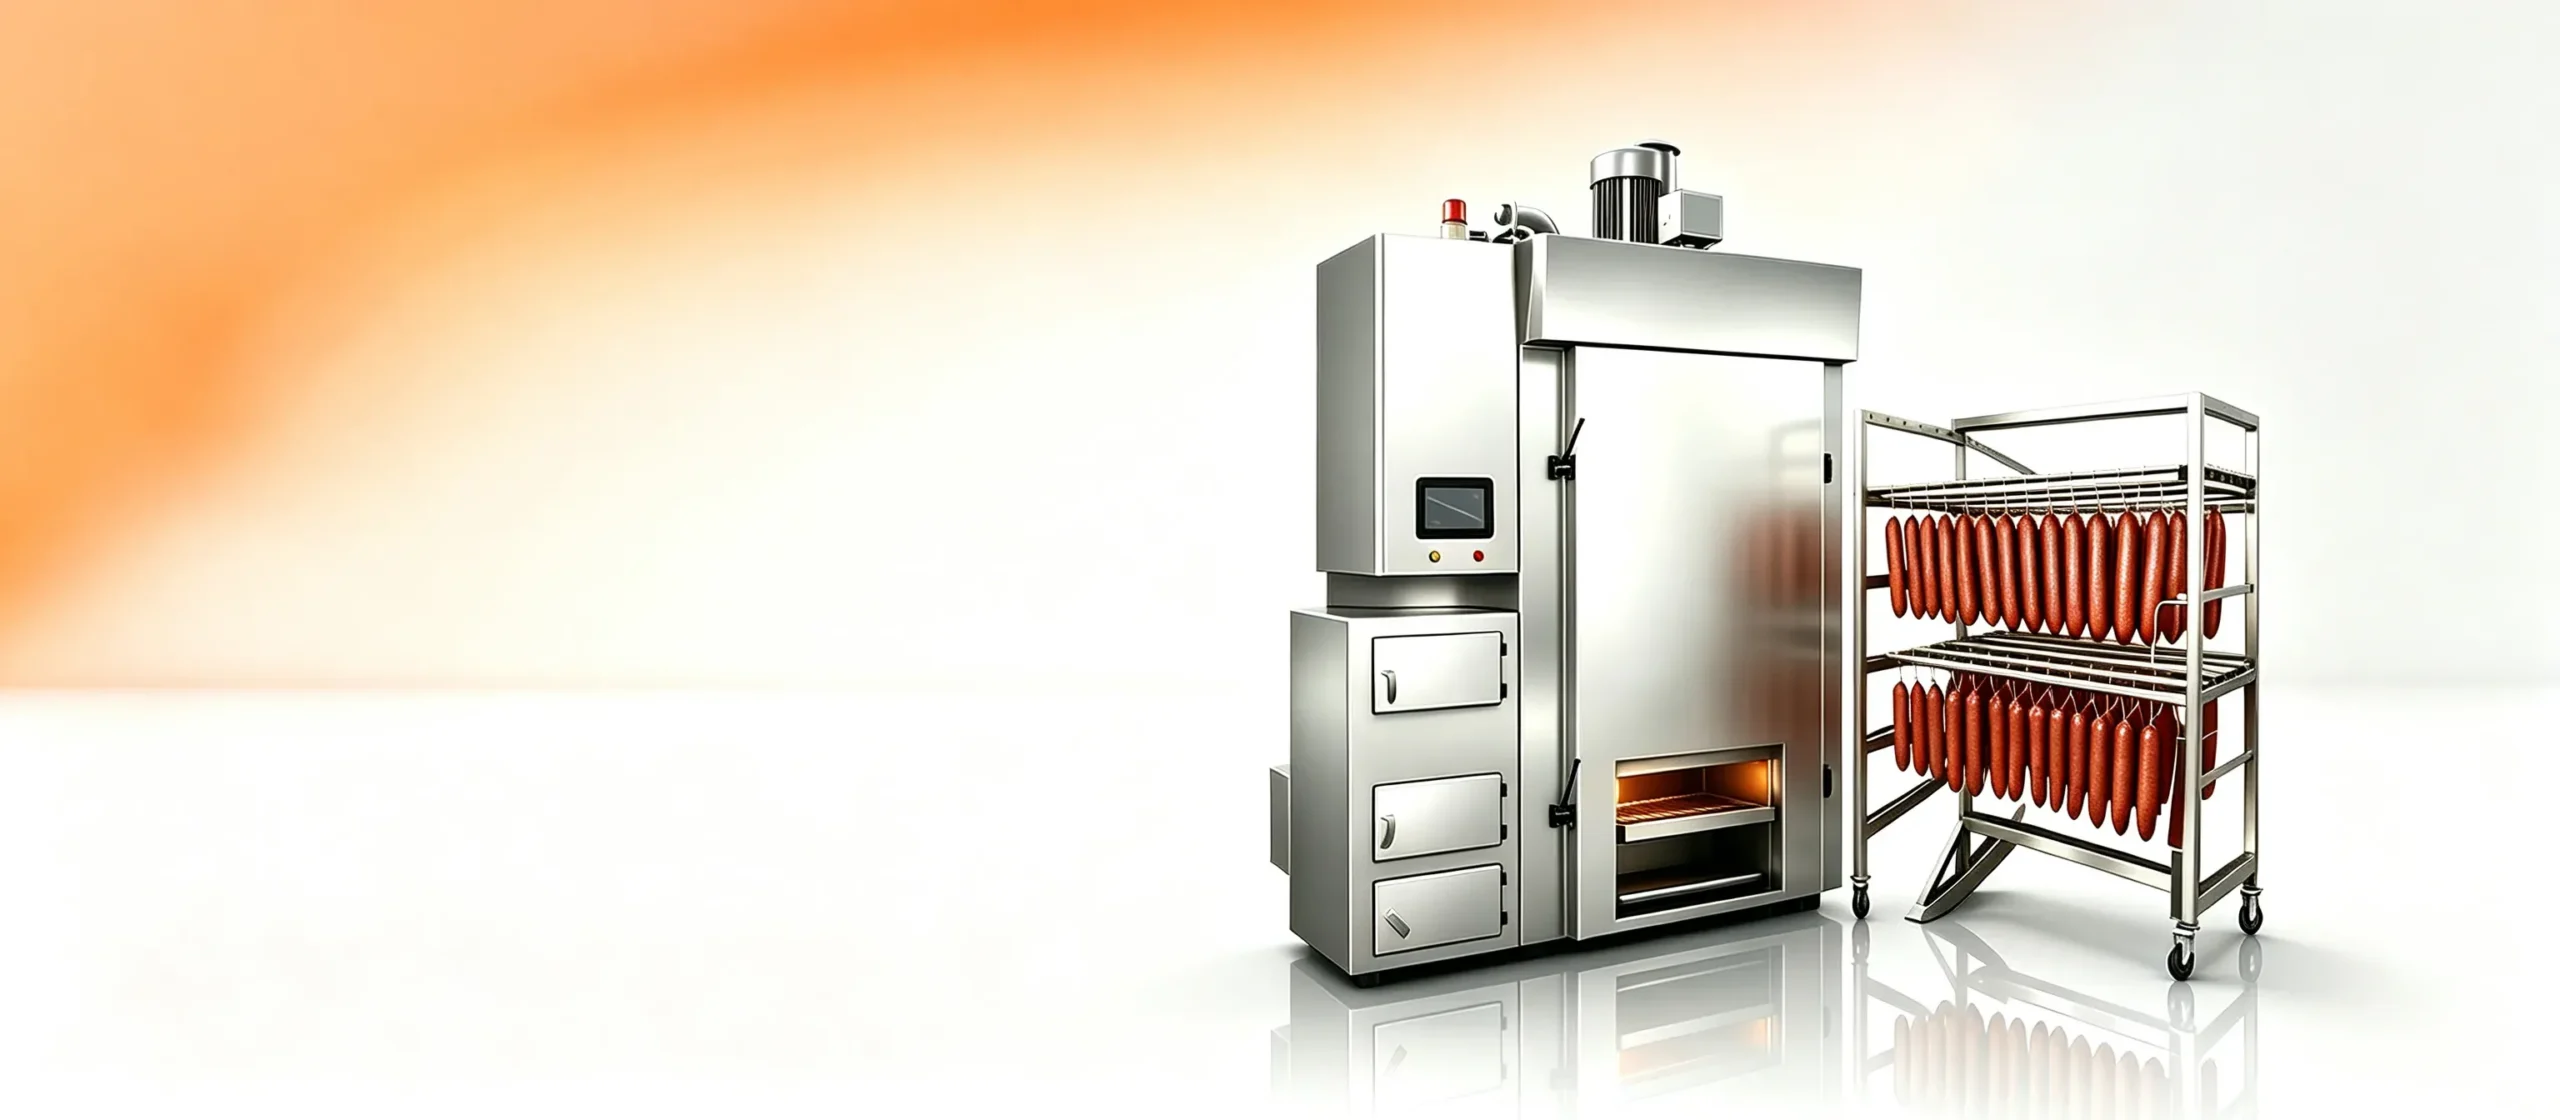
A hydraulic sausage stuffer operates on a batch displacement principle: a hydraulic ram forces a fixed cylinder of meat paste toward the nozzle. Output is inherently pulsed — when the cylinder is empty, the ram retracts, the cylinder refills, and only then does filling resume. This creates a production gap of 15–45 seconds per refill cycle, during which the downstream line (clipping, hanging) continues running or must stop.
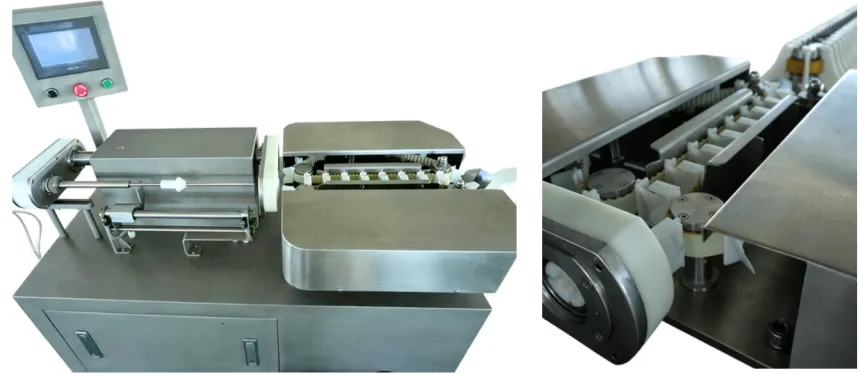
A vacuum filler operates on continuous rotary displacement: the vane rotor turns without interruption, drawing paste from the hopper and delivering it to the nozzle in a quasi-continuous stream. There is no batch cycle and no production gap — the only interruption is hopper loading, which with automated feeding systems occurs in under 30 seconds and does not require a full production stop.
Throughput Comparison at Industrial Scale
| Performance Factor | Vacuum Filler (Vane-Type) | Hydraulic Sausage Stuffer |
|---|---|---|
| Maximum throughput | 3,000–6,500 kg/h (continuous) | 800–2,500 kg/h (batch-limited) |
| Effective throughput (incl. refill downtime) | 93–98% of nameplate | 65–80% of nameplate |
| Weight deviation (±g per link) | ±0.8–1.5g (encoder-controlled) | ±2–5g (pressure-dependent) |
| Filling pressure consistency | ±0.02 bar (servo-controlled) | ±0.3–0.8 bar (hydraulic variation) |
| Air pocket incidence | Very low (dual-stage vacuum) | Moderate to high (no vacuum stage) |
| Casing type compatibility | All types at all speeds | Better suited to robust casings |
| Shift output (8h, 22mm frankfurter) | 25,000–50,000+ links | 8,000–18,000 links |
| Automation compatibility | Full PLC integration, servo sync | Limited — typically manual stop/start |
Weight Consistency: Where the Gap Is Largest
For hot dog and frankfurter production, portion weight consistency directly determines retail pack accuracy and give-away cost. Hydraulic stuffers produce pressure curves that vary across the cylinder stroke — higher at full cylinder, lower as the cylinder empties — creating a characteristic weight gradient across each batch cycle. Links filled at the start of a batch are typically 3–6% heavier than those at the end.
Vacuum fillers with encoder-controlled portioning deliver the same displacement volume on every cycle, regardless of where in the hopper cycle the machine is operating. The ±0.8–1.5g deviation achievable with a servo-controlled vane filler represents 5–8× better weight consistency than a hydraulic stuffer operating at equivalent throughput — a difference that is immediately visible in retail pack over-weight audits.
Air Pockets and Product Quality
Hydraulic stuffers have no vacuum stage. Paste is loaded into the cylinder under atmospheric conditions, and any air mixed in during grinding, tumbling, or hopper loading travels directly into the casing. Air pocket incidence on hydraulic stuffers typically runs 2–5% of links at high speed — a significant quality issue for hot dogs, where a single visible void in a cooked product triggers retail returns.
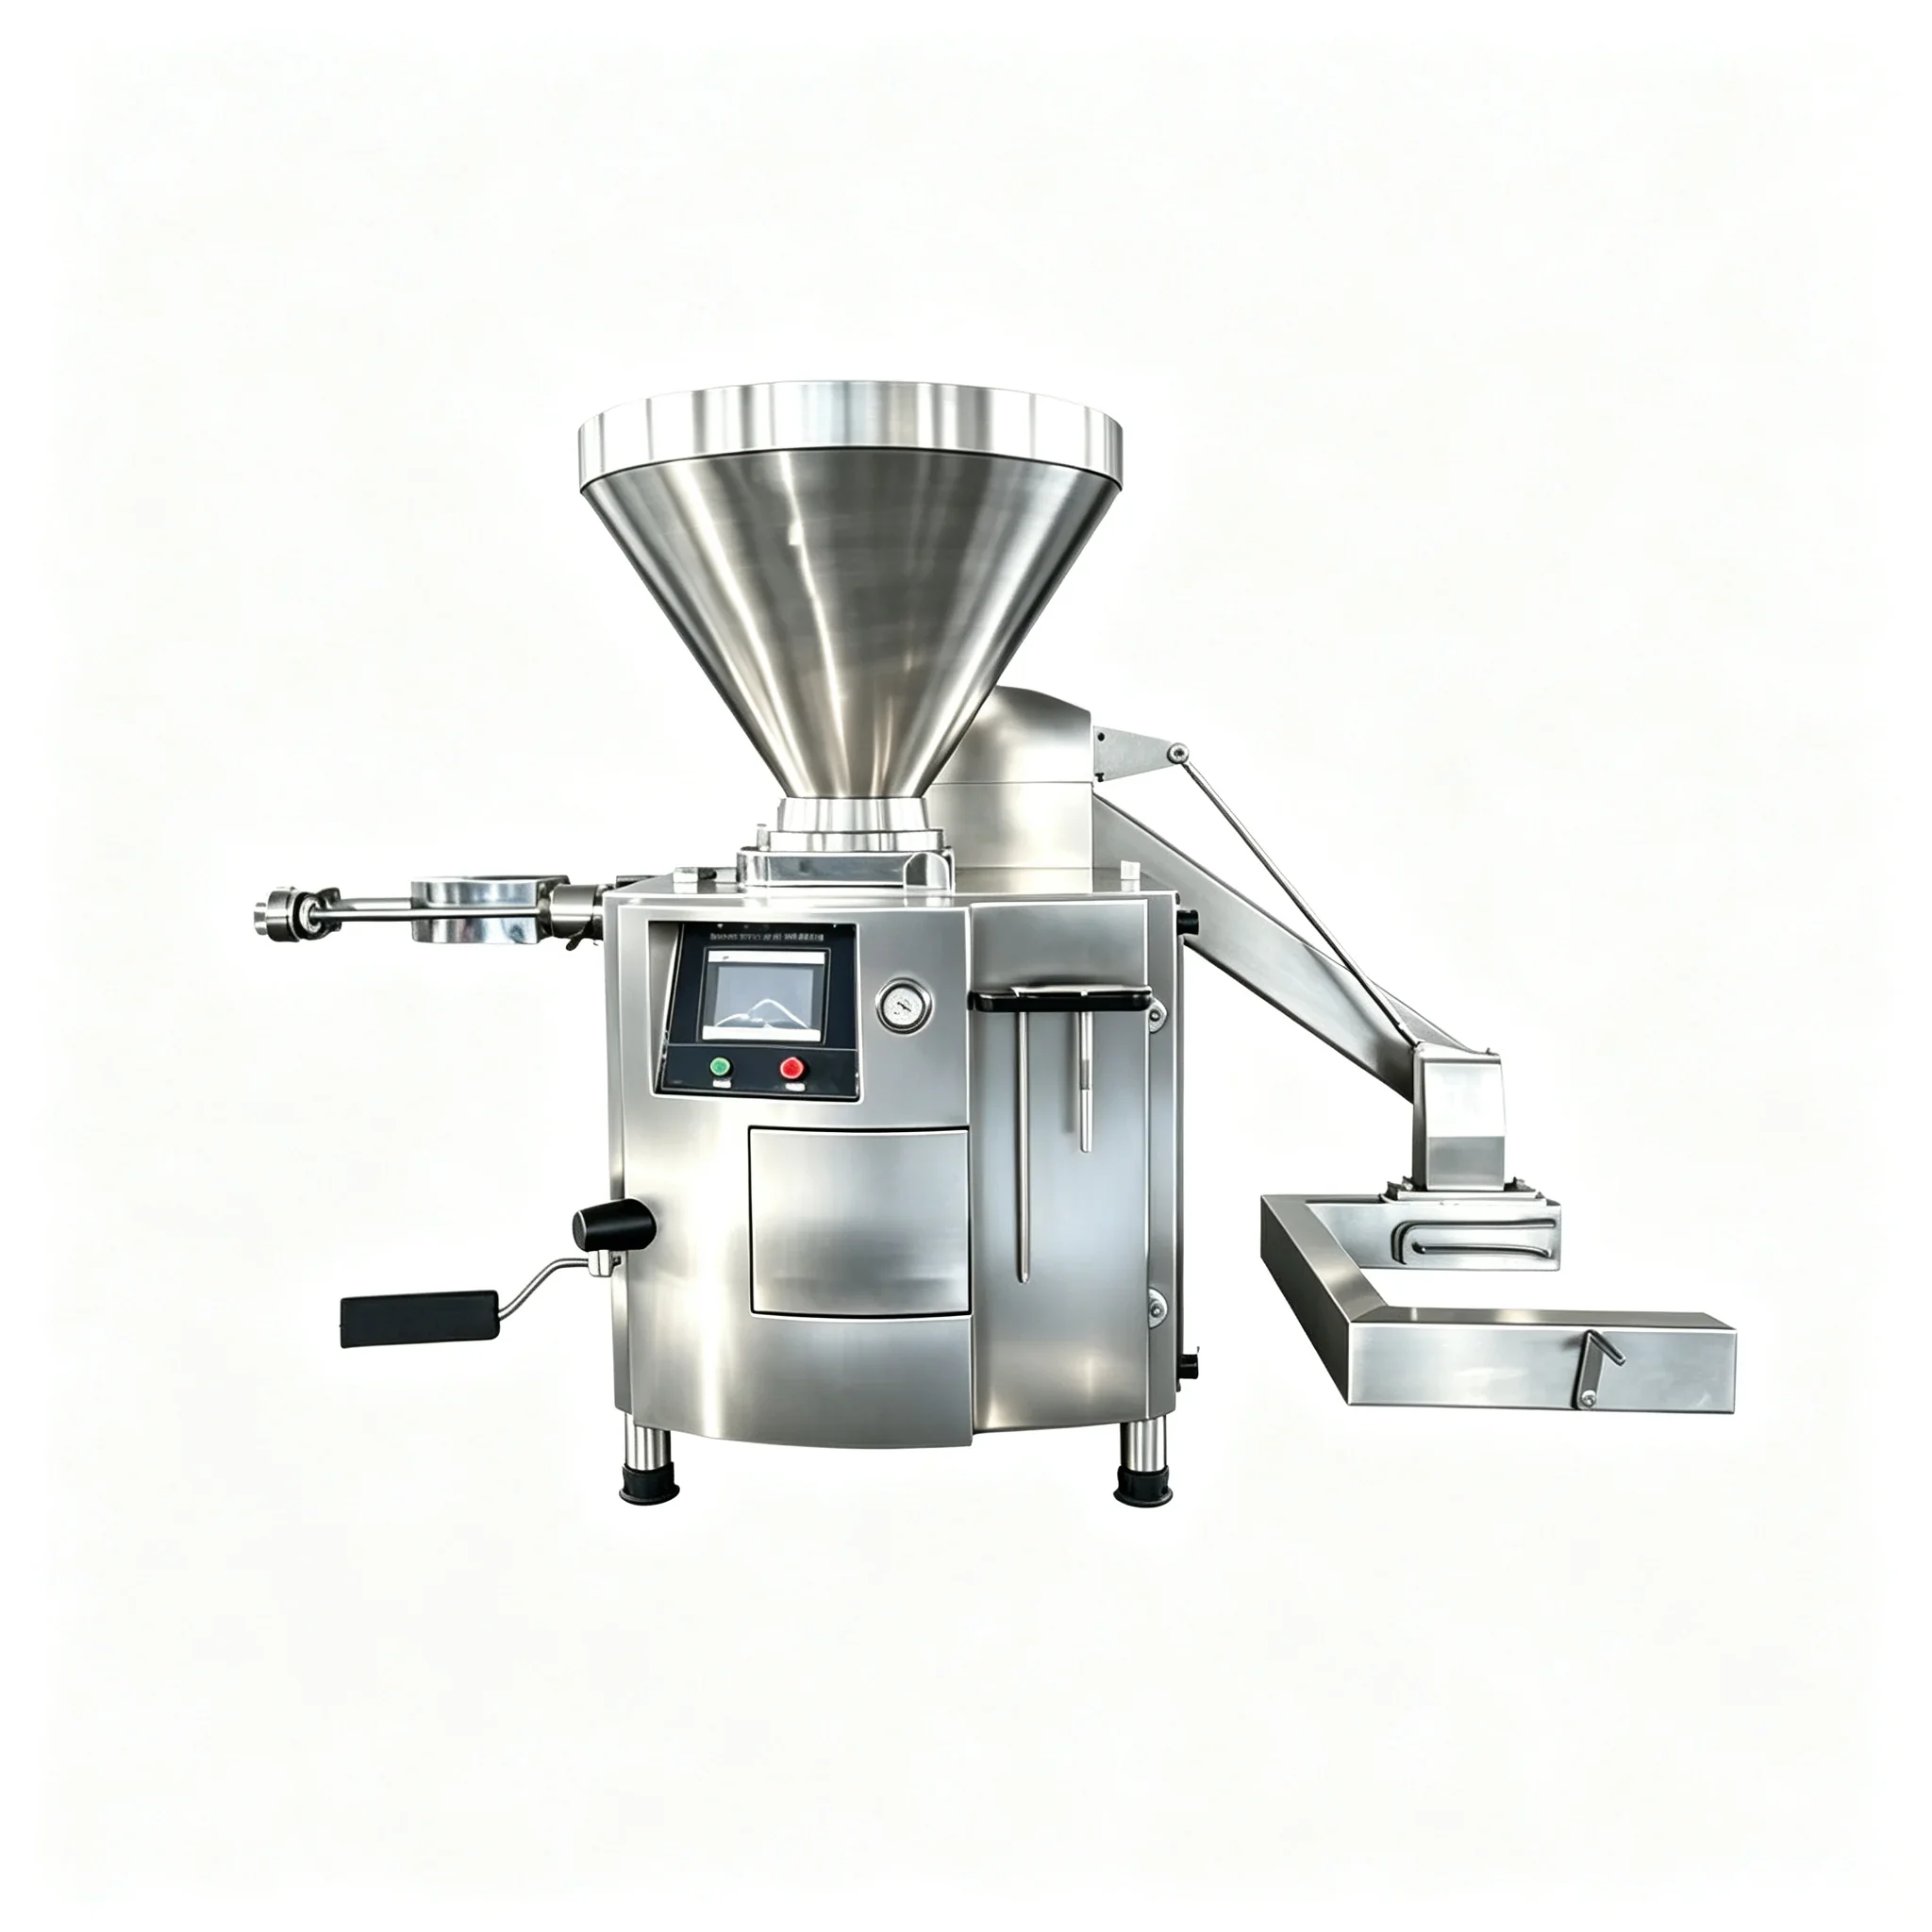
The ZKG-6500 vacuum filling machine maintains dual-stage vacuum at −0.085 MPa sustained, reducing air pocket incidence to below 0.1% of links under normal operating conditions. For retail-packaged hot dogs and frankfurters, where pack presentation is a commercial requirement, this difference is not marginal — it is the difference between acceptable and rejected product.
Automation and Line Integration
Modern hot dog production lines are automated from filler to packing — the filler, clipping or linking unit, hanging conveyor, smokehouse trolley loading, chiller, and packaging line all operate under shared PLC control. Vacuum fillers are designed from the ground up for this architecture: they have servo drives with external speed reference inputs, PLC communication ports (CANopen, Profinet, EtherCAT), and interlock I/O for fault signalling.
Hydraulic stuffers, by contrast, are fundamentally batch machines. Their control architecture is based on hydraulic circuit logic — pressure-switched valves, manual speed control, and batch-cycle timers. Integrating a hydraulic stuffer into a PLC-controlled line requires significant custom engineering that typically costs more than the price differential between the two machine types, and the resulting integration is always a compromise.
Where Hydraulic Stuffers Still Have a Role
Hydraulic stuffers are not obsolete for every application. They remain well-suited to: craft and artisan sausage production where batch sizes are small and product variety is high, facilities producing emulsified or whole-muscle deli products in large-diameter fibrous casings (60mm+) where continuous-flow vacuum filling offers diminishing returns, and operations where capital budget severely constrains the equipment specification and throughput targets are below 1,500 kg/h.
For industrial hot dog and frankfurter production at volumes above 1,500 kg/h, however, the operational case for hydraulic stuffers is difficult to make on any metric: throughput, weight consistency, air pocket control, automation compatibility, or effective output per shift. The vacuum sausage filler wins on all five.
Total Cost of Ownership: Beyond the Sticker Price
Give-Away Reduction
At ±1.5g vs ±4g deviation, a 6,500 kg/h vacuum filler saves 2.5g average give-away per link. At 50,000 links/shift, that is 125kg of product per shift — at commodity sausage value, significant annual savings.
Maintenance Cost
Hydraulic stuffers require hydraulic oil changes, seal replacements, and ram cylinder service. Vacuum fillers require vane replacement every 3,000–3,500h. Total maintenance cost per tonne of output is comparable; vacuum fillers require less unplanned downtime.
Rejection Rate
Air pocket-driven retail rejections on hydraulic-stuffed hot dogs are a recurring cost rarely attributed to the filler. Eliminating 80–90% of air pockets with vacuum filling directly reduces retail returns and rework costs.
Labour Cost
Hydraulic stuffers require an operator for cylinder loading and refill monitoring. Automated vacuum fillers with lift-and-tip hopper loading run with one operator supervising multiple machines.
Ready to Optimise Your Sausage Production Line?
Send us your output targets and casing spec — we respond within 48 hours.
+86 13083988828 | ✉ [email protected]