Weight deviation is the hidden enemy of high-speed sausage production. At 20,000+ links per hour, a deviation of just ±3g per link translates to several hundred kilograms of give-away product per shift — or, worse, under-weight packs that trigger retail rejection. Achieving a consistent sausage weight deviation of ±1g at industrial throughput requires precision at three stages: filling, portioning control, and line synchronisation. This guide covers each one.
Why Weight Deviation Occurs at High Speed
At low production speeds, mechanical irregularities in a sausage filler are self-correcting — the system has enough dwell time to recover between cycles. At 5,000–6,500 kg/h, that margin disappears. Every millisecond of rotor hesitation, every viscosity shift in the meat paste, and every back-pressure spike from the casing line translates directly into a measurable weight variance at the link.
The most common root causes fall into three categories: equipment-related, material-related, and process-related. Understanding which category your deviation originates from is the first step toward bringing it within ±1g.
Rotor Speed Fluctuation
Mechanical cam or hydraulic piston systems produce sinusoidal output — inherently cyclic deviation that worsens as speed increases.
Paste Viscosity Shift
Temperature changes of just 2°C in the meat paste alter flow resistance enough to change fill volume per cycle by 1.5–2.5%.
Back-Pressure from Linker
If the linking or hanging line speed lags the filler even momentarily, casing back-pressure reduces fill volume at the nozzle for that cycle group.
Casing Caliber Variation
Collagen casing lot-to-lot diameter tolerance of ±0.3 mm changes the internal volume per link length, shifting apparent weight even when fill volume is constant.
The Role of Encoder-Controlled Portioning
The single most impactful upgrade for weight deviation control is replacing cam-based portioning with encoder-controlled volumetric portioning. In a cam system, fill volume per cycle is set mechanically — and it cannot compensate for paste viscosity changes or pressure variations in real time. An encoder-based system reads actual rotor displacement and adjusts motor torque on every cycle to maintain a target displacement volume, regardless of what the paste is doing.
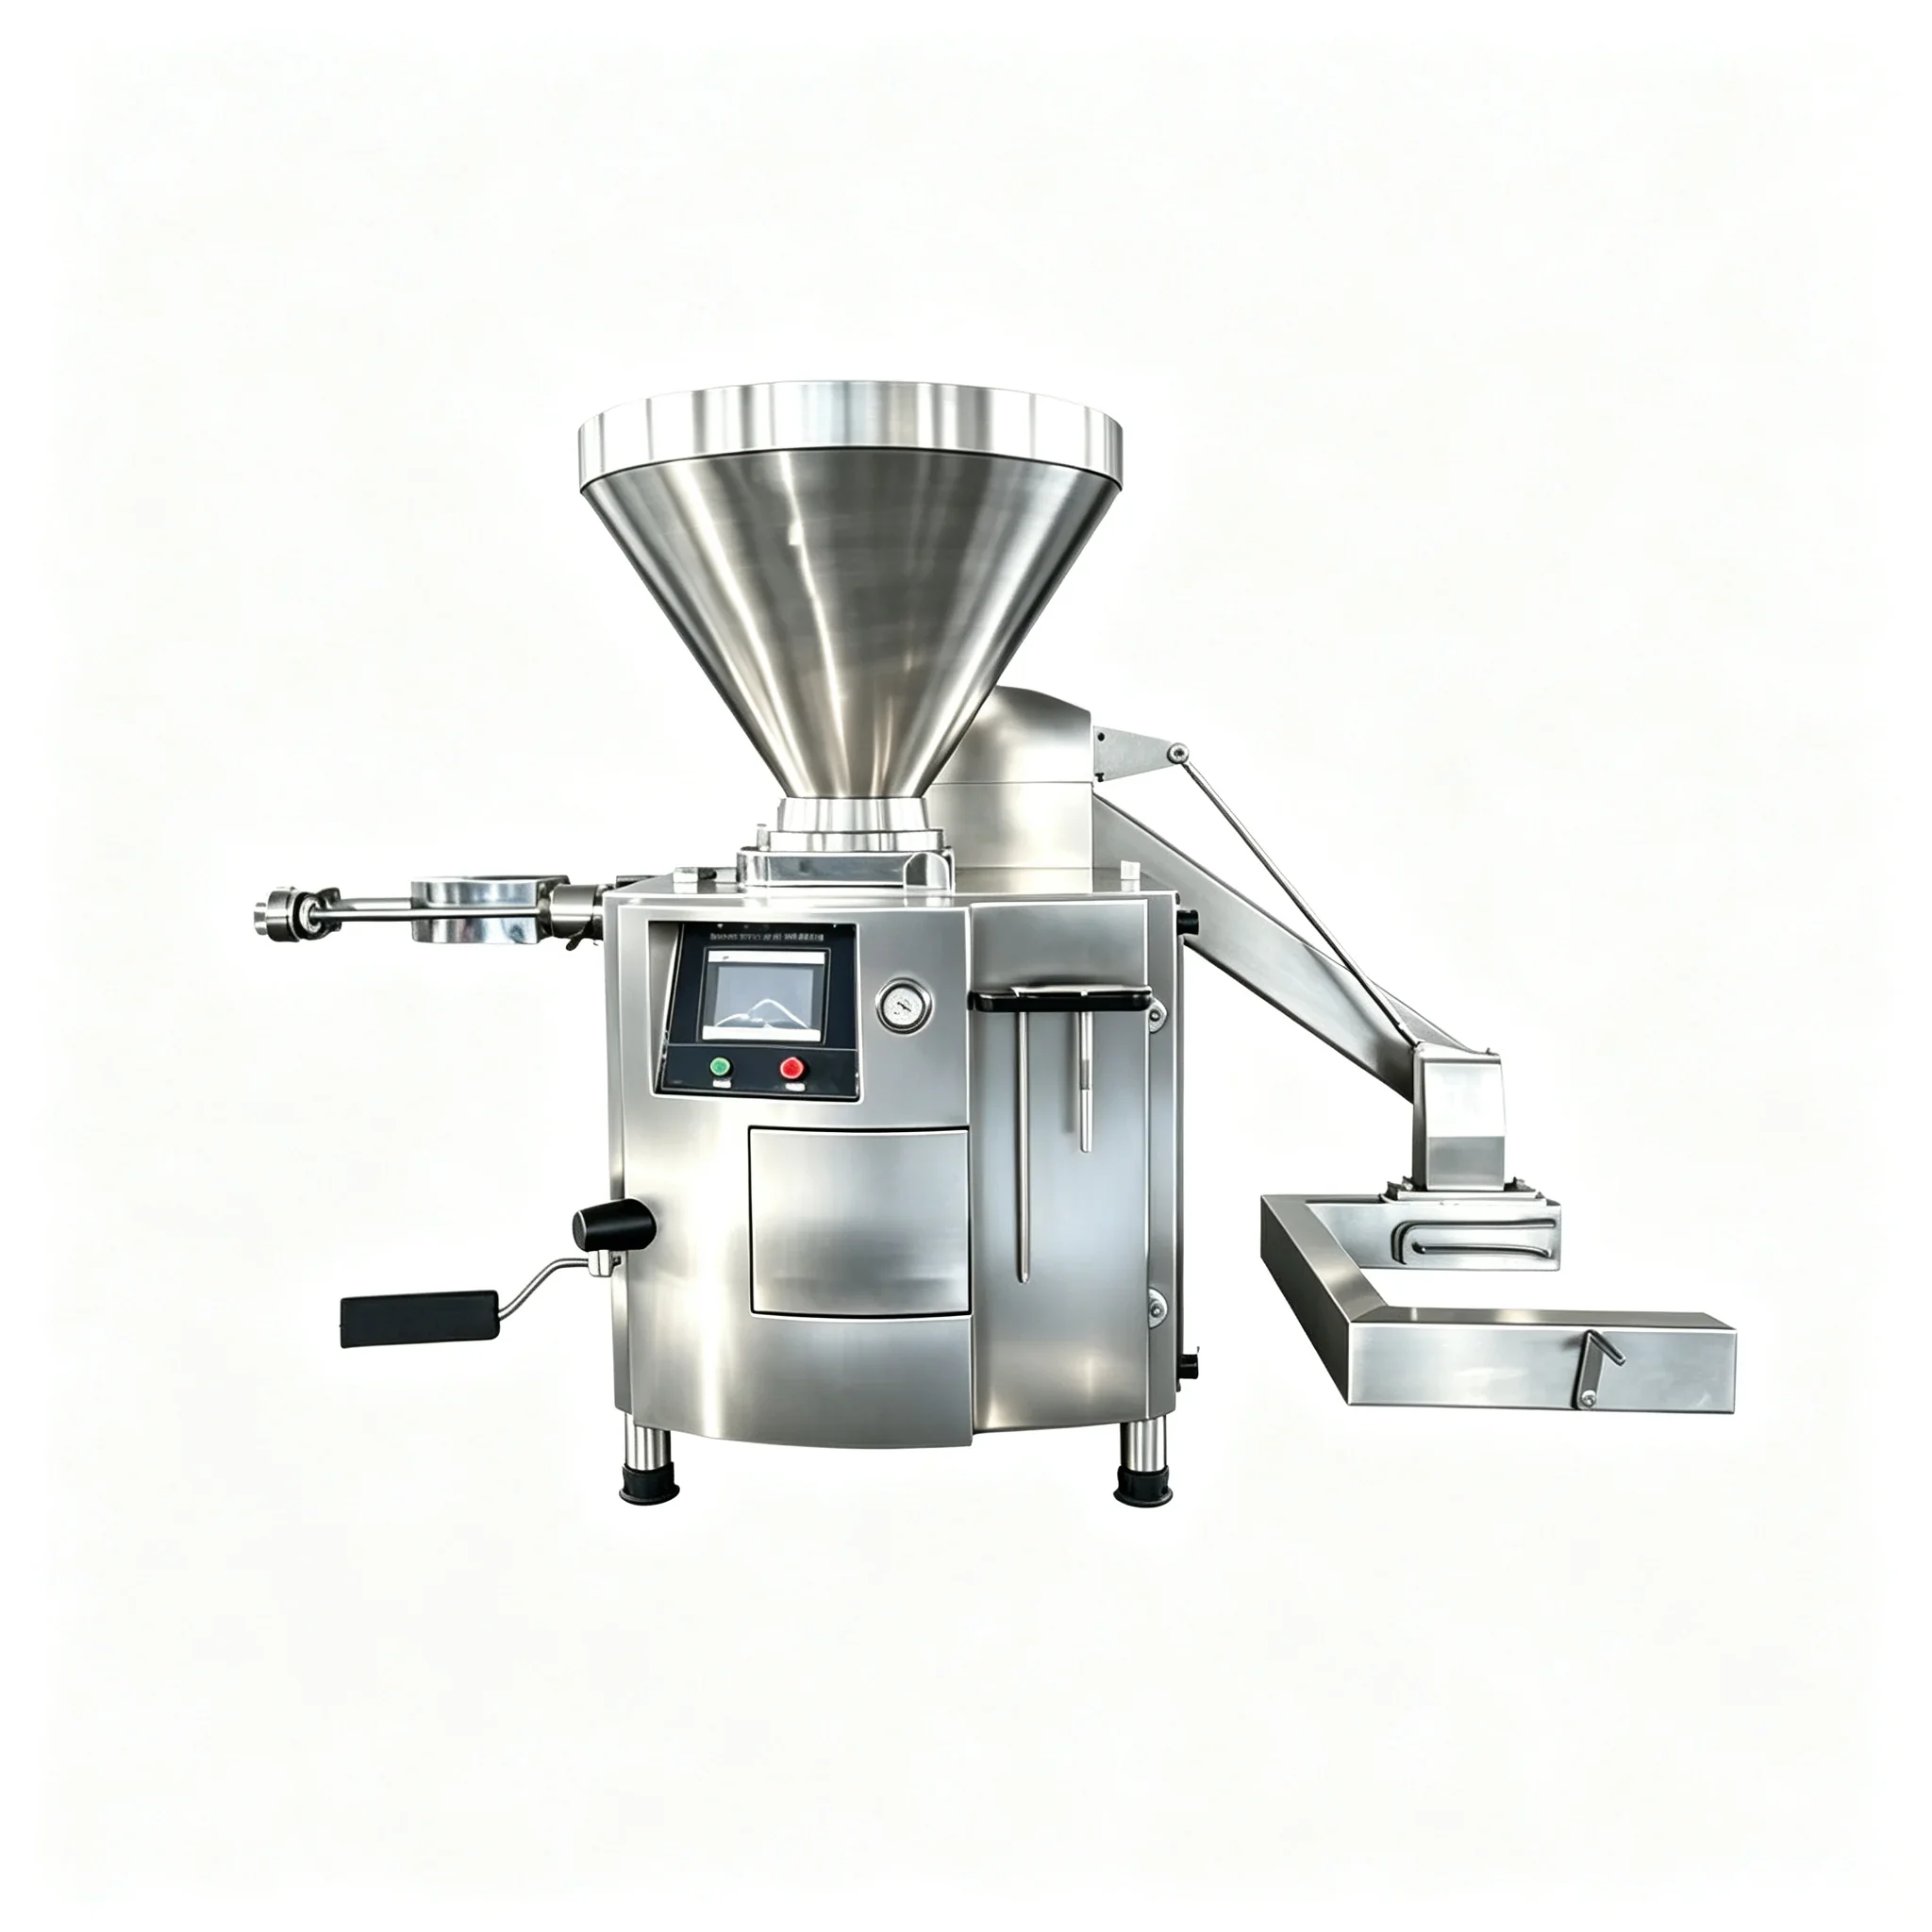
The ZKG-6500 vacuum filling machine uses pulse-encoder portioning with a resolution of 0.1° of rotor arc — equivalent to approximately 0.8ml of fill volume per increment. At typical frankfurter weights of 50–80g, this gives a mechanical repeatability floor of ±0.4g before any process variables are considered. Achieving ±1g in production requires controlling those process variables on top of this mechanical foundation.
Material Preparation: The Upstream Factor Most Plants Ignore
Weight consistency at the filler depends heavily on what arrives in the hopper. Paste that varies in temperature, fat content, or air content between hopper loads will produce weight deviation even on a mechanically perfect machine — because the volumetric displacement that the encoder measures is not the same as the weight delivered when density fluctuates.
Temperature Control
Keep meat paste between −1°C and +2°C at the point it enters the filler hopper. Above +3°C, fat begins to smear rather than distribute evenly, reducing bulk density and causing the encoder to over-deliver weight per cycle. Below −2°C, viscosity rises sharply and the vacuum system works harder, which can cause micro-bubbles that further reduce delivered weight.
Vacuum Mixing Consistency
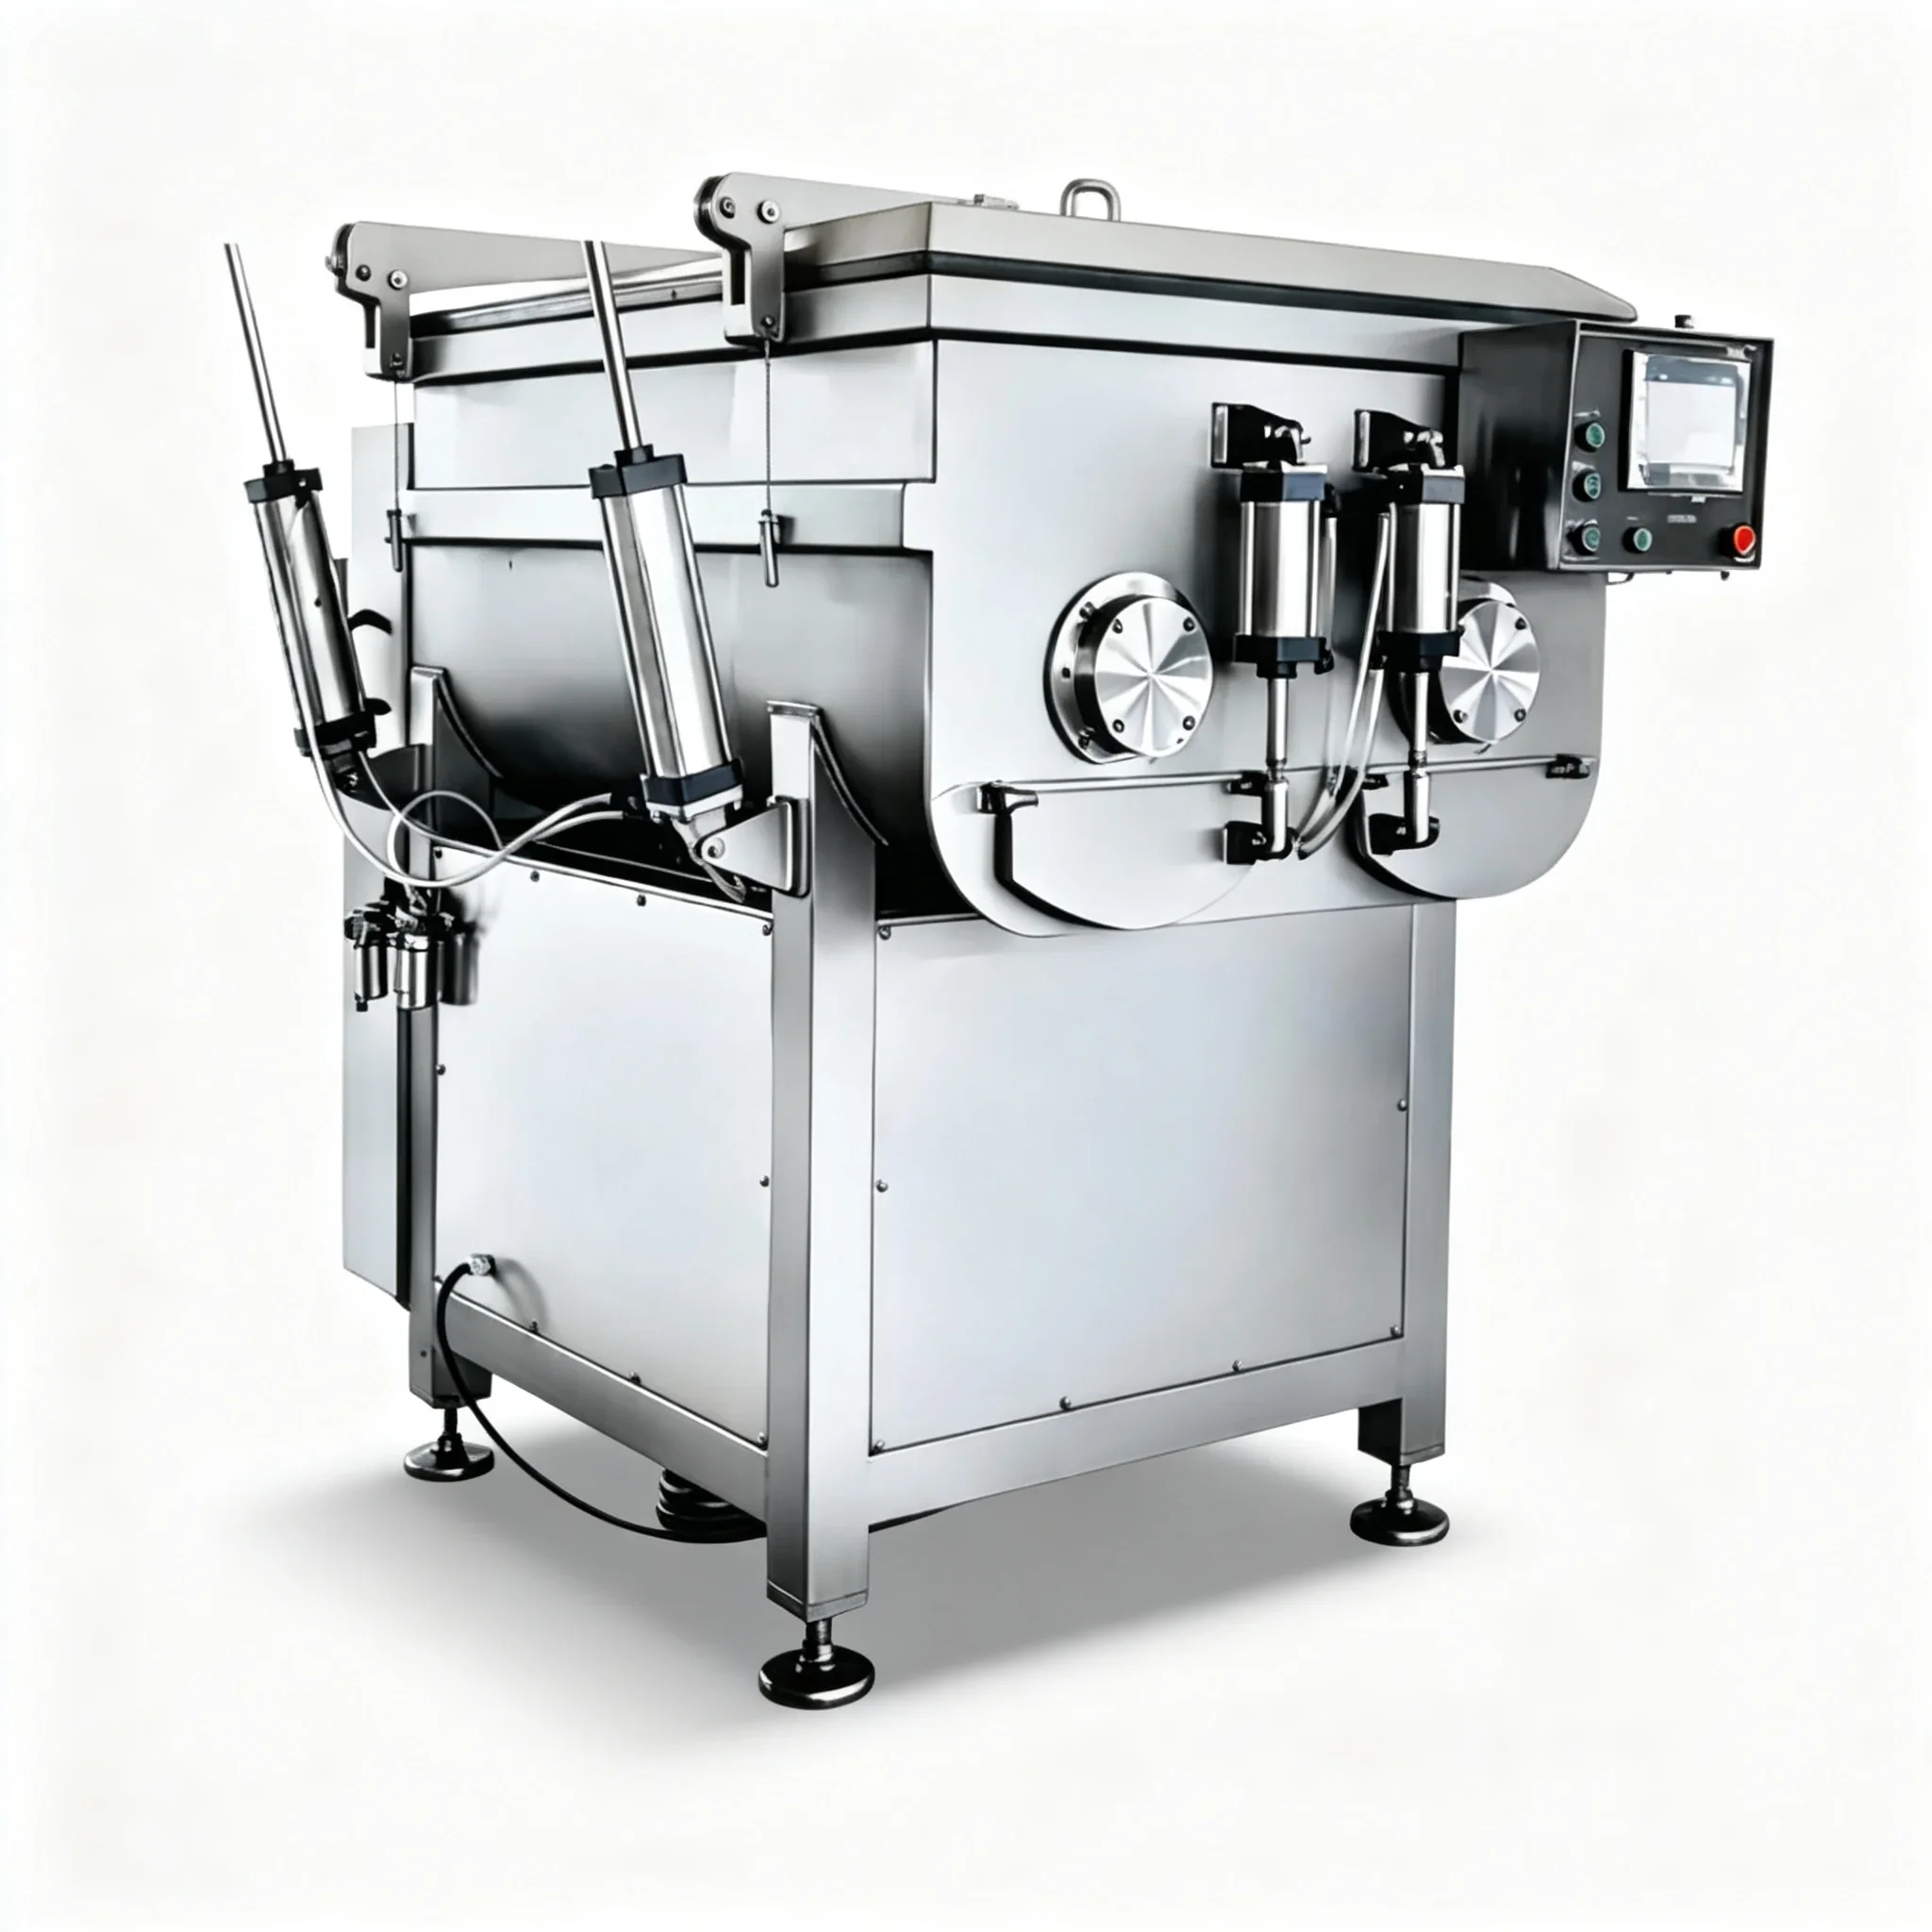
Batches mixed under inconsistent vacuum levels arrive at the filler with variable air content. A batch at 40% of target vacuum carries significantly more entrained air than one at 95% — and that air compresses during filling, reducing weight delivered per cycle. Running a JB-Series vacuum mixer at a consistent −0.085 MPa for the full mix duration removes this variable from the weight equation.
Line Synchronisation: Matching Filler to Clipping or Linking Speed
A filler operating at rated throughput while the downstream clipping or linking unit runs 3–5% slower creates a progressive back-pressure condition at the nozzle. Back-pressure is not uniform — it builds over 8–12 cycles, then releases when the casing slack is taken up. This produces a characteristic batch pattern in weight data: a run of 8–12 links progressively under-weight, followed by 2–3 links over-weight as pressure releases.
The fix is shared PLC speed reference between the filler and the automatic sausage hanging line, so both units accelerate and decelerate together. Any speed correction applied at the filler must propagate to the downstream unit within one fill cycle (typically 80–150ms at high speed) to prevent back-pressure build-up.
| Source of Deviation | Typical Magnitude | Detection Method | Corrective Action |
|---|---|---|---|
| Encoder portioning error | ±0.4–0.8g | Statistical process control (SPC) | Encoder calibration, vane wear check |
| Paste viscosity shift | ±0.6–1.8g | Temperature log vs weight log correlation | Hopper temperature monitoring, tighter temp control |
| Back-pressure from linker | ±0.8–2.2g (cyclic) | Pattern in weight data (8–12 link cycles) | PLC speed sync, reduce linker lag |
| Casing caliber variation | ±0.5–1.2g | Weight variation correlated with casing lot change | Tighter casing supplier spec, lot verification |
| Air content variation | ±0.4–1.0g | Bubble count in vacuum gauge log | Consistent vacuum mixing protocol |
In-Line Checkweigher Integration
Closed-loop weight control — where a checkweigher downstream feeds live weight data back to the filler’s portioning controller — can hold ±1g deviation even when upstream process variables drift. The checkweigher samples every link or every nth link and computes a running average; the portioning controller adjusts encoder target displacement in response. This setup requires that the filler accept an analogue or digital weight correction signal, which modern servo-controlled fillers support as a standard input.
Without a checkweigher integration, the practical floor for sustained ±1g accuracy requires: paste temperature within ±1°C, vacuum mixing at consistent target vacuum, casing from a single lot per production run, and PLC-synchronised downstream line speed. Most plants can achieve this with process discipline and proper equipment specification.
Why Choose Our Filling Equipment
Our vacuum filling machines are engineered for the precision demands of industrial sausage production. Manufactured at our facility in Hangzhou and run-tested at full throughput before shipment, each machine is configured with encoder-controlled portioning, dual-stage vacuum, and servo drive as standard — not optional extras. Contact our team at [email protected] or via the contact page to discuss your weight accuracy requirements.
Ready to Optimise Your Sausage Production Line?
Send us your output targets and casing spec — we respond within 48 hours.
+86 13083988828 | ✉ [email protected]